- admin@youerfilms.com
- Mon - Sat at 9:00AM to 18:00PM
Leave Your Message
🛡️ The intersection of heavy industrial manufacturing and stringent health regulations has birthed a revolutionary application in packaging: utilizing PVC Food Film for Industrial Machinery Protection. Traditionally, industrial machines were coated in thick, petroleum-based greases or wrapped in standard, non-regulated plastics to prevent oxidation and physical damage during transit or downtime. However, as global supply chains evolve, particularly within the food processing, pharmaceutical, and high-precision electronics sectors, these antiquated methods are no longer sufficient. The modern industrial landscape demands protective layers that are not only robust against environmental stressors but also chemically inert, non-toxic, and compliant with international health standards.
Currently, the global market for industrial protective films is experiencing a massive paradigm shift. Regulatory bodies across North America, Europe, and Asia are tightening the rules regarding what materials can come into contact with machinery used for human consumption products. If a multi-million-dollar food processing line is shipped overseas wrapped in standard industrial plastic, the off-gassing and chemical leaching from that plastic can contaminate the stainless steel surfaces. When the machinery is commissioned, these micro-contaminants can transfer to food products, leading to catastrophic recalls and health hazards.
This is where food-grade PVC film steps in as an indispensable commercial asset. Engineered to meet FDA and EU food contact regulations, this specialized film provides the high tensile strength required for heavy machinery while guaranteeing zero toxic residue. Industrial manufacturers are increasingly adopting this material not just as a compliance measure, but as a competitive advantage. Selling a state-of-the-art beverage bottling machine wrapped in certified food-grade PVC communicates to the end-buyer an uncompromising commitment to quality and safety from the factory floor to the installation site.
⚙️ The versatility of PVC Food Film for Industrial Machinery Protection extends far beyond simple dust covers. By leveraging its unique molecular structure—which offers exceptional cling, puncture resistance, and an impermeable moisture barrier—engineers have integrated this film into highly specific and demanding industrial scenarios.
In the dairy, meat packing, and bakery industries, equipment must undergo rigorous washdowns using caustic chemicals and high-pressure hot water. When these production lines are paused for maintenance, retrofitting, or factory relocation, protecting the sensitive internal components (like conveyor belts, mixing vats, and extrusion nozzles) is critical. Wrapping these components in food-grade PVC film ensures that no airborne factory dust, moisture, or stray industrial lubricants contaminate the sanitized surfaces. Because the film is inherently food-safe, any accidental contact with the processing areas requires minimal re-sanitization compared to industrial-grade wraps.
Pharmaceutical machinery operates in ISO-certified cleanrooms. The introduction of any foreign particulate can ruin entire batches of life-saving medications. When transporting pill presses, blister packaging machines, or liquid filling stations into these cleanrooms, the machinery must be wrapped in materials that do not shed microplastics or release volatile organic compounds (VOCs). High-transparency, food-grade PVC film acts as the perfect sterile barrier. It allows technicians to visually inspect the machinery through the wrap before moving it into the cleanroom, minimizing the time the equipment is exposed to unconditioned air during the unwrapping process.
Exporting heavy machinery across oceans exposes equipment to one of nature's most corrosive elements: salt-laden sea air. Traditional anti-corrosion methods involve coating the machine in heavy cosmoline or grease, which takes hours of labor and harsh solvents to remove upon arrival. By utilizing heavy-duty, multi-layered PVC food film, logistics companies can create a hermetic seal around the machinery. The superior cling properties of the film eliminate air pockets where condensation could form, while the robust polymer chain blocks salt molecules from reaching the metal. Upon arrival, the film is simply sliced away, leaving a pristine, ready-to-operate machine without the need for toxic degreasers.
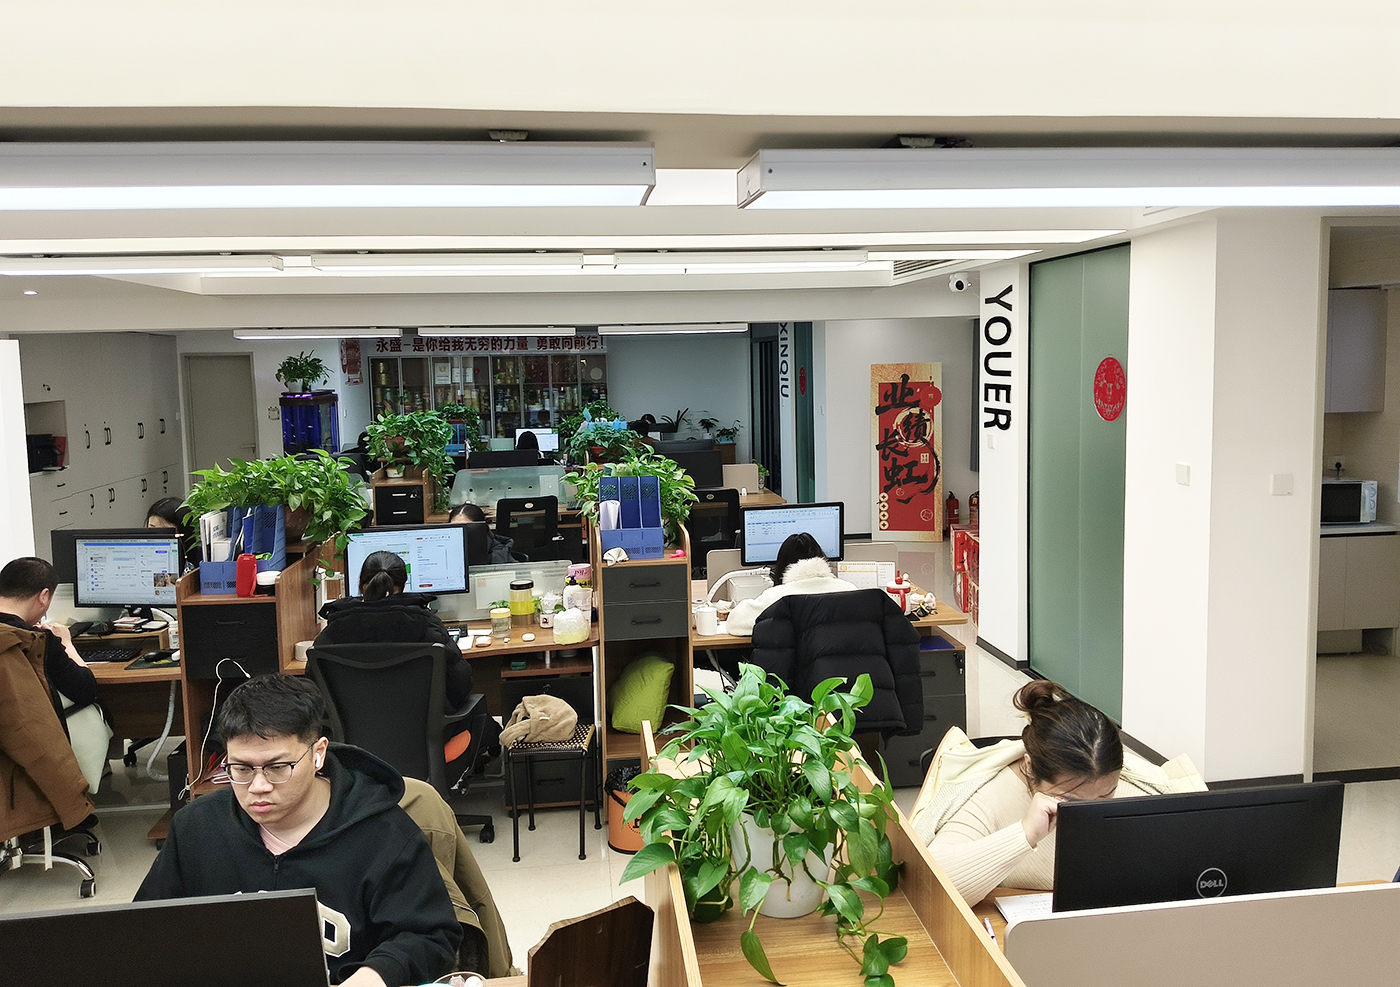
Hebei Youer New Material Science and Technology Co., Ltd. has been founded since 2007. It is located in Shijiazhuang City, Hebei Province, and has specialized in film for more than 10 years and becomes a modern high-tech enterprises integrating R & D, production and sales.
Our product system focuses on three core product lines — stretch film, protective film and BOPP film, with detailed extended classifications to fully cover the diverse application needs of various industries.
With experience in product development and materials exporting, we have gained a very good reputation among customers from more than 80 countries. Our professional sales team which is always ready to give quick response, provide multi choice to satisfy customer requirements with one stop service.
🚀 As global industry marches towards Industry 4.0 and stricter environmental, social, and governance (ESG) standards, the development of PVC Food Film for Industrial Machinery Protection is not remaining stagnant. The future of this specialized packaging material lies at the intersection of nanotechnology, smart materials, and ecological sustainability.
One of the most significant trends is the push for sustainability. While traditional PVC provides unmatched protection, the end-of-life disposal of massive industrial wraps poses an environmental challenge. Industry leaders are now investing heavily in research to blend food-grade PVC with Polylactic Acid (PLA) and other biodegradable polymers. The goal is to create a film that maintains its structural integrity and moisture barrier properties during the months-long transit and storage of machinery, but can be broken down efficiently in industrial composting facilities post-use. This shift will allow heavy machinery manufacturers to dramatically reduce their carbon footprint and appeal to eco-conscious global buyers.
The next frontier in machinery protection is "Smart Film." Imagine a roll of PVC food-grade film embedded with nano-sensors or color-changing chemical indicators. If a piece of precision machinery is wrapped and sealed, the film could change color from transparent blue to bright red if the internal humidity exceeds a certain threshold, alerting warehouse managers to a potential breach in the seal before rust can form. Similarly, impact-sensitive films could highlight areas where the machinery was struck by a forklift during transit, providing undeniable visual proof for insurance claims. By integrating these tech-forward features, PVC film evolves from a passive protective layer into an active logistics monitoring tool.
In conclusion, optimizing the protection of vital industrial assets requires materials that offer uncompromising strength and absolute chemical safety. By choosing advanced food-grade PVC films, industries can safeguard their multi-million-dollar investments, ensure regulatory compliance, and streamline their global logistics operations.
We strictly implement international quality control standards throughout the entire production process, from the selection of high-quality raw materials to the precision testing of finished products, forming a complete quality management system. Every roll of film leaving the factory has undergone strict inspection to ensure that it meets the highest quality requirements of customers.
We have built a professional R&D team composed of senior engineers and technical talents, equipped with advanced R&D and testing equipment. We focus on technological breakthroughs and product upgrading, and continuously develop environmentally friendly, efficient and high-performance film products to keep pace with the changing market demand and lead the industry development trend.
Our vision is to become a world-class film manufacturer, promote the sustainable development of the film industry, and create greater value for customers, employees and society through continuous innovation and unremitting efforts. We are looking forward to build up a long term partnership with more and more potential customers all over the world.
Recognized globally for our commitment to quality and innovation in industrial film manufacturing.