- admin@youerfilms.com
- Mon - Sat at 9:00AM to 18:00PM
Leave Your Message
Explore our top-tier packaging films designed for optimal load retention, clarity, and industrial efficiency in the food and beverage sector.
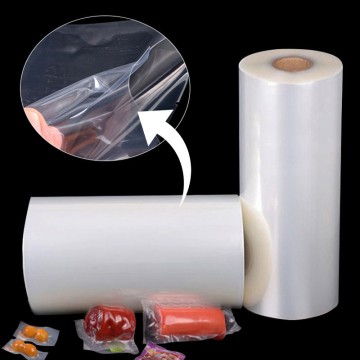
In the highly competitive and fast-paced world of Fast-Moving Consumer Goods (FMCG), the significance of robust, reliable, and aesthetically pleasing packaging cannot be overstated. Among the myriad of materials available, PE Wrapping Film For Food And Beverage Multipacks has emerged as the undisputed champion. Polyethylene (PE) film, specifically engineered for collation and shrink wrapping, provides the perfect synergy of mechanical strength, optical clarity, and cost-efficiency. Whether it is a six-pack of craft beer, a 24-pack of bottled mineral water, or bulk-canned vegetables, PE wrapping film ensures that products remain secure from the manufacturing line to the consumer's pantry.
The commercial and industrial landscape for PE wrapping films has undergone a massive transformation over the last decade. Historically, packaging relied heavily on corrugated cardboard boxes or polyvinyl chloride (PVC) films. However, the paradigm has shifted dramatically. Corrugated cardboard, while recyclable, adds significant weight and volume to shipments, thereby increasing logistics costs and carbon footprints. PVC, on the other hand, poses severe environmental and health risks during its lifecycle, particularly concerning chloride emissions during incineration. Consequently, global regulatory bodies and environmentally conscious corporations have aggressively pivoted towards Polyethylene (PE) solutions. PE films are lighter, highly customizable, and crucially, 100% recyclable within the #4 LDPE/LLDPE recycling streams. The modern industrial status of PE wrapping film is characterized by a relentless drive towards thinner gauges (down-gauging) without compromising tensile strength, a feat made possible by advanced multi-layer co-extrusion technologies.
The global market for shrink and stretch films is experiencing exponential growth, driven primarily by the food and beverage sector. Modern retail environments demand packaging that not only protects but also acts as a silent salesman. PE wrapping films used for multipacks are now frequently printed with high-definition graphics, utilizing flexographic or rotogravure printing techniques. This transforms a simple collation film into a vibrant billboard, enhancing brand visibility on supermarket shelves. Furthermore, the rise of e-commerce and direct-to-consumer grocery deliveries has necessitated secondary packaging that can withstand the rigors of individual parcel shipping. PE films offer superior puncture resistance and "bullseye" closures that provide convenient carrying handles for consumers, bridging the gap between industrial utility and consumer convenience.
From a commercial standpoint, manufacturers are intensely focused on Total Cost of Ownership (TCO). High-performance PE wrapping films allow beverage companies to run their packaging lines at unprecedented speeds—often exceeding 100 packs per minute. The consistency of the film's slip properties and its low-temperature shrink profiles reduce energy consumption in shrink tunnels, translating to massive cost savings and a lower environmental impact over annual production cycles.
The most ubiquitous application for PE Wrapping Film For Food And Beverage Multipacks is in the beverage industry. Bottled water and carbonated soft drinks require extremely tight unitization to prevent shifting during transit. PE shrink film is engineered to shrink uniformly in both the machine direction (MD) and transverse direction (TD). When a 24-pack of PET water bottles passes through a heat tunnel, the PE film contracts, creating a rigid, brick-like structure. This structural integrity is vital for palletization. Modern PE films are formulated with metallocene polyethylene (mPE), which drastically improves the dart impact strength and tear resistance. This means that even if a consumer accidentally drops a multipack, the film will stretch rather than shatter, preventing product loss. Furthermore, for the brewing industry, opaque or UV-resistant PE films are often utilized to protect light-sensitive craft beers from "skunking" (photochemical degradation) while still providing the benefits of multipack unitization.
Beyond beverages, canned goods such as soups, beans, and pet foods rely heavily on PE wrapping films. Unlike bottles, tinplate or aluminum cans have sharp rims (chimes) that can easily slice through inferior packaging materials. High-performance PE films are specifically extruded with a tough outer layer to resist these abrasions. In the dairy sector, where multipacks of yogurt cups or flavored milk cartons are common, hygiene and temperature control are paramount. PE films provide an excellent moisture barrier, preventing condensation in refrigerated environments from degrading the secondary packaging. This is a crucial advantage over cardboard, which loses its structural integrity when exposed to moisture in cold-chain logistics.
The frozen food industry presents a unique set of challenges for packaging materials. Standard plastics can become brittle and fracture at sub-zero temperatures. However, specialized PE formulations, including blends with PEVA (Polyethylene Vinyl Acetate), are designed to maintain their elasticity and toughness even in deep-freeze environments. This ensures that multipacks of frozen vegetables, meats, or ice cream remain securely bundled from the frozen warehouse, through refrigerated transport, right to the supermarket freezer display. The anti-fog properties often incorporated into these films also ensure that condensation does not obscure the branding or barcode readability.
Hebei Youer New Material Science and Technology Co., Ltd. has been founded since 2007. It is located in Shijiazhuang City, Hebei Province, and has specialized in film for more than 10 years and becomes a modern high-tech enterprises integrating R & D, production and sales.
Our product system focuses on three core product lines — stretch film, protective film and BOPP film, with detailed extended classifications to fully cover the diverse application needs of various industries, especially in the realm of PE Wrapping Film For Food And Beverage Multipacks.
With experience in product development and materials exporting, we have gained a very good reputation among customers from more than 80 countries. Our professional sales team which is always ready to give quick response, provide multi choice to satisfy customer requirements with one stop service.
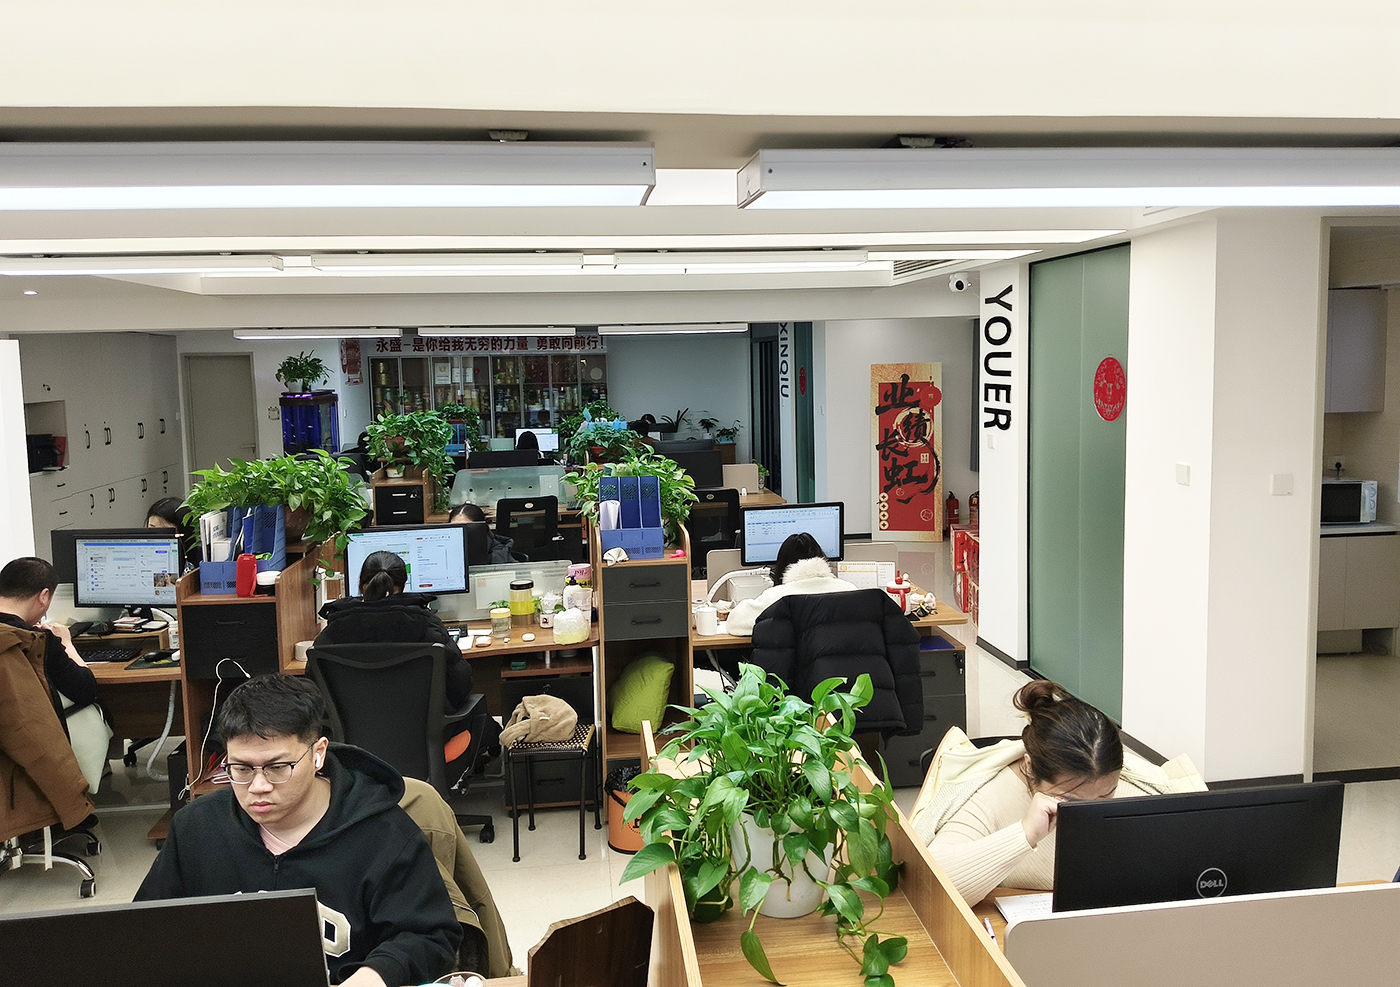
We strictly implement international quality control standards throughout the entire production process, from the selection of high-quality raw materials to the precision testing of finished products, forming a complete quality management system. Every roll of film leaving the factory has undergone strict inspection to ensure that it meets the highest quality requirements of customers.
We have built a professional R&D team composed of senior engineers and technical talents, equipped with advanced R&D and testing equipment. We focus on technological breakthroughs and product upgrading, and continuously develop environmentally friendly, efficient and high-performance film products to keep pace with the changing market demand.
Our vision is to become a world-class film manufacturer, promote the sustainable development of the film industry, and create greater value for customers, employees and society through continuous innovation and unremitting efforts. We are looking forward to build up a long term partnership with more and more potential customers all over the world.
As we look toward the future of PE Wrapping Film For Food And Beverage Multipacks, two massive megatrends are reshaping the industry: Artificial Intelligence (AI) integration in manufacturing, and the uncompromising push for sustainability. The intersection of these two forces is creating a new paradigm of "Smart Packaging."
The extrusion of PE films is a highly complex thermodynamic process. Variables such as melt temperature, die pressure, ambient humidity, and cooling rates must be perfectly synchronized to produce a film with uniform thickness and predictable shrink properties. Today, cutting-edge manufacturers are deploying AI-powered predictive maintenance and real-time process optimization. Machine learning algorithms analyze thousands of data points per second from sensors on the extrusion lines. If the AI detects a microscopic deviation in film gauge, it can autonomously adjust the die lips in milliseconds, ensuring zero-defect production. Furthermore, computer vision systems powered by deep learning are used for inline quality inspection, detecting gels, pinholes, or print defects at line speeds that human operators could never monitor. This AI integration not only reduces waste but ensures that beverage companies receive flawlessly consistent PE wrapping film, eliminating costly downtime on their high-speed packaging lines.
The environmental impact of single-use plastics is the most pressing issue in the packaging sector. The future of PE wrapping film lies in circular economy models. We are witnessing a massive surge in the development of films incorporating Post-Consumer Recycled (PCR) resins. Advanced compatibilizers and AI-assisted polymer blending allow manufacturers to incorporate up to 50% PCR material into shrink films without a significant drop in mechanical performance or optical clarity. This drastically reduces the reliance on virgin fossil fuels and lowers the carbon footprint of beverage multipacks.
In parallel, the industry is exploring bio-based and biodegradable alternatives. Innovations such as Soft PLA (Polylactic Acid) food-grade cling films are paving the way for compostable secondary packaging. While traditional PE remains the standard for heavy-duty multipacks due to its unmatched strength-to-weight ratio, the continuous refinement of polymer science is bridging the gap. Innovations in catalyst technology are yielding "mono-material" packaging designs, ensuring that the PE wrapping film, the printed labels, and even the adhesives are all compatible within the same recycling stream, making the recycling process effortless for consumers and municipal waste facilities alike.
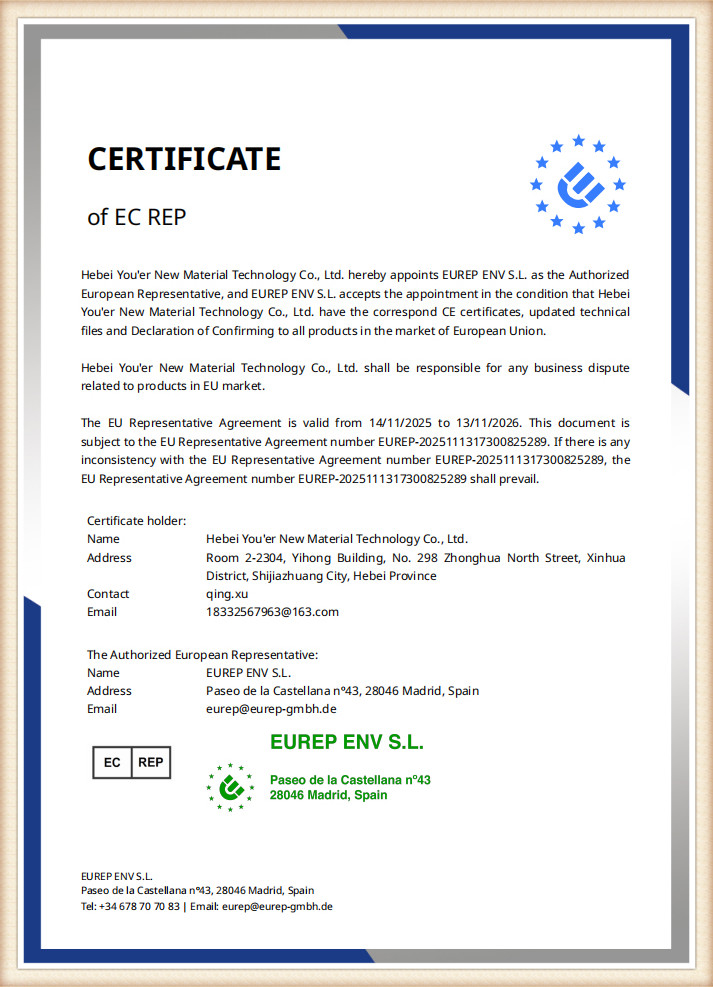
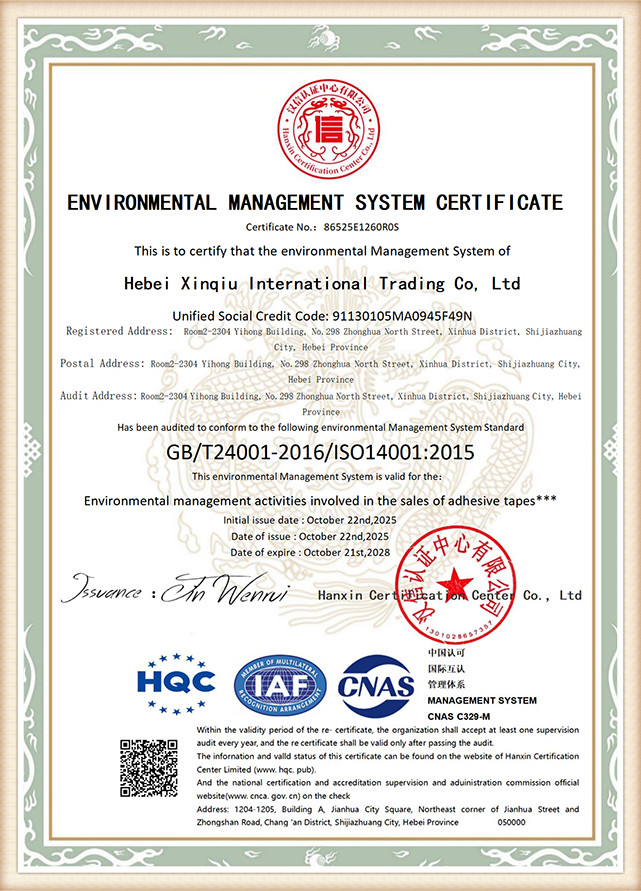
Showcasing our innovations in PE Wrapping Film For Food And Beverage Multipacks on the global stage, backed by internationally recognized certifications.
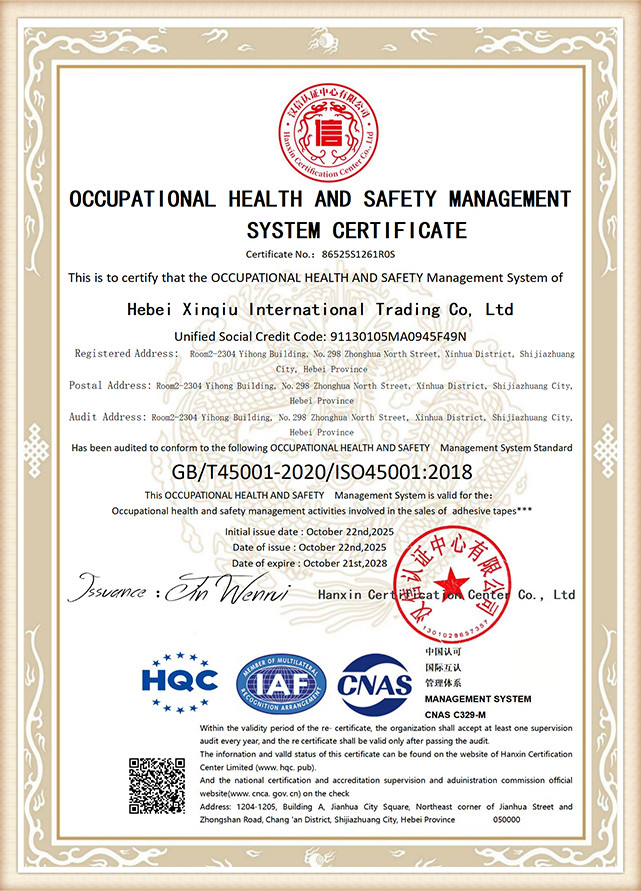
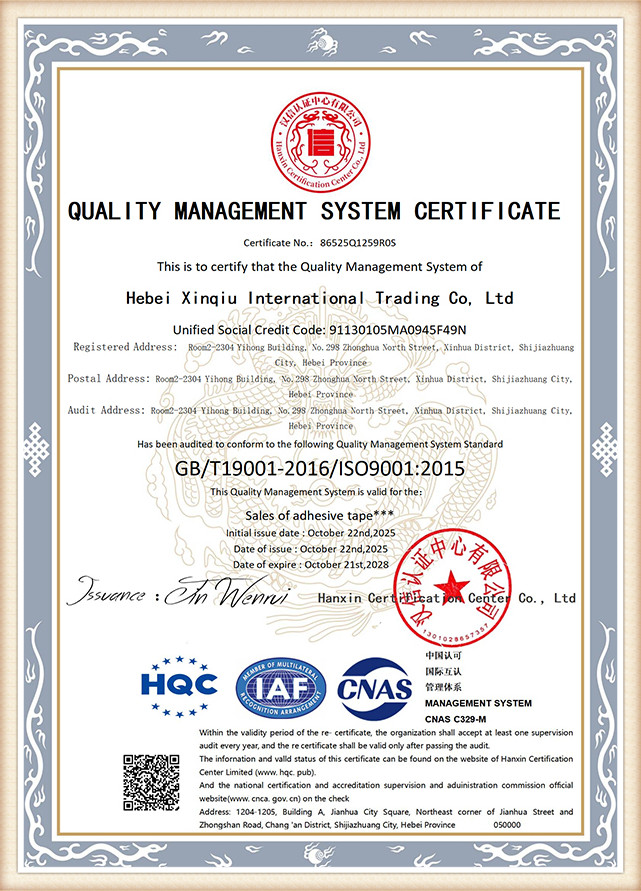
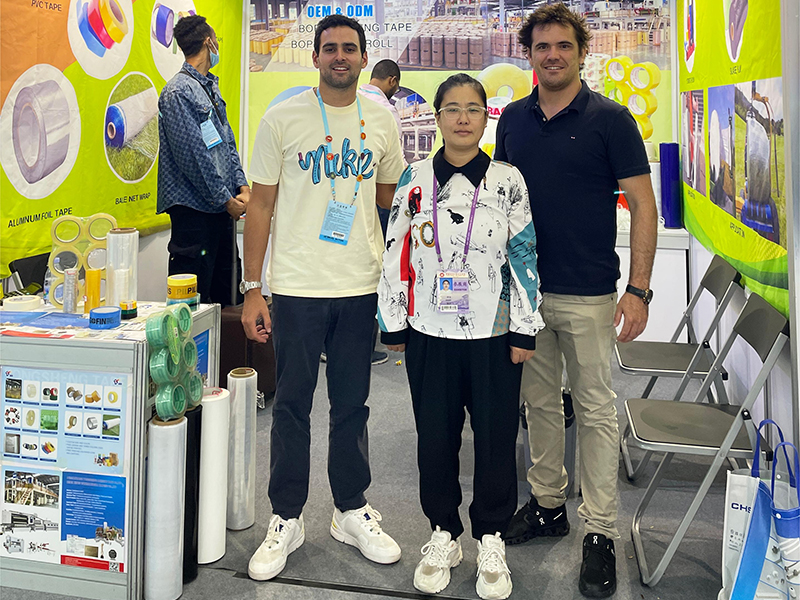
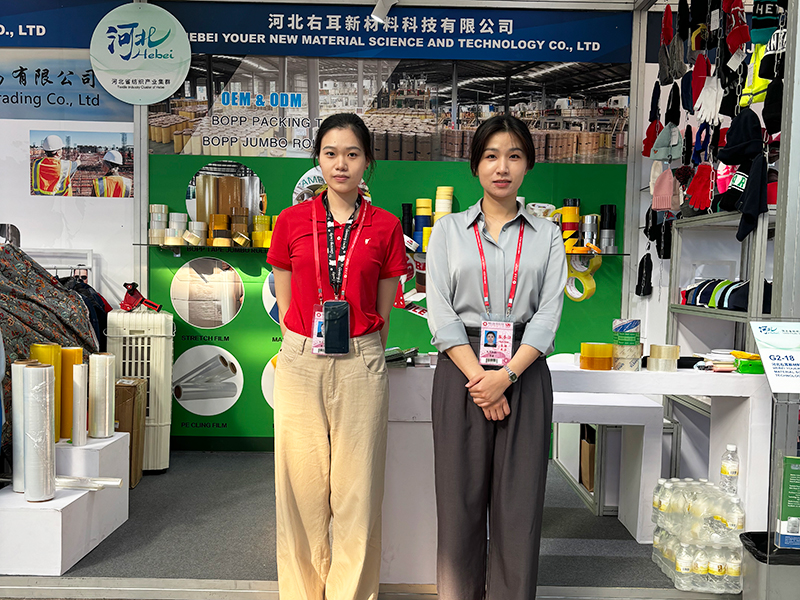
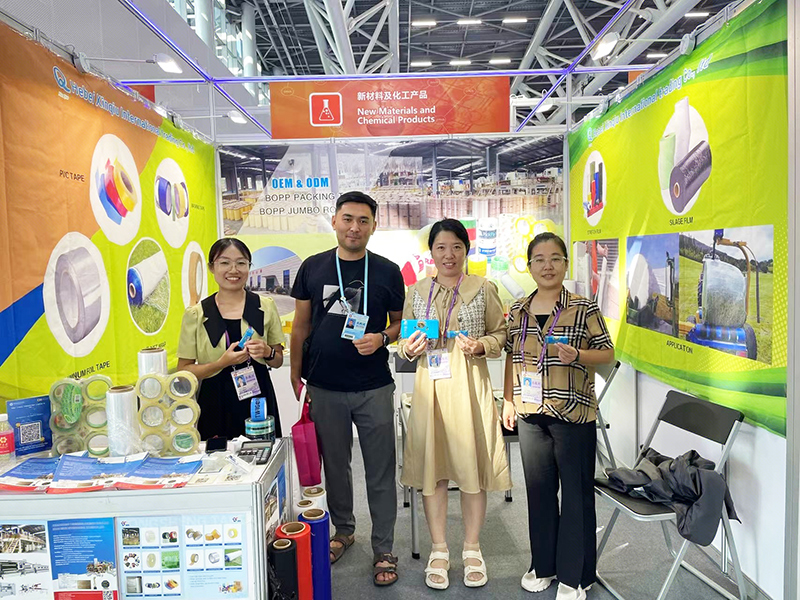
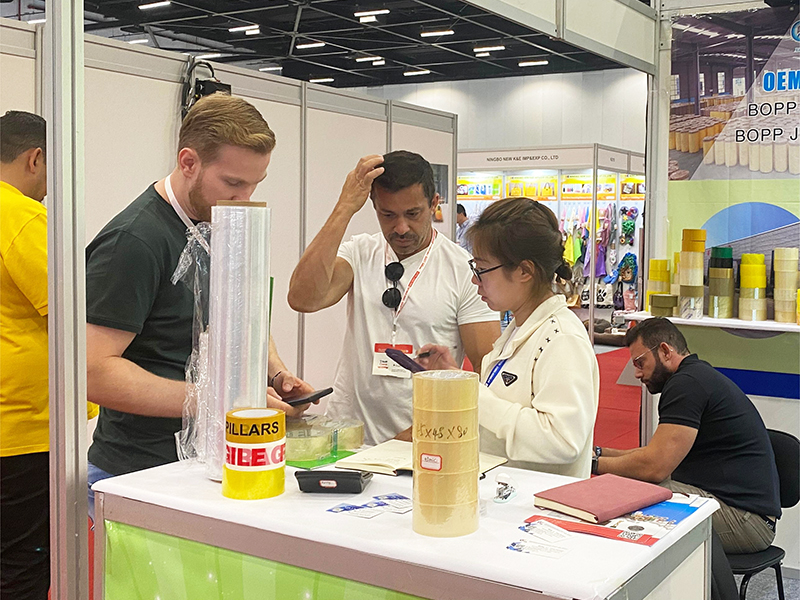
From advanced PE heat shrink films to specialized protective and biodegradable solutions, discover our full range of innovative materials engineered for modern industrial demands.