- admin@youerfilms.com
- Mon - Sat at 9:00AM to 18:00PM
Leave Your Message
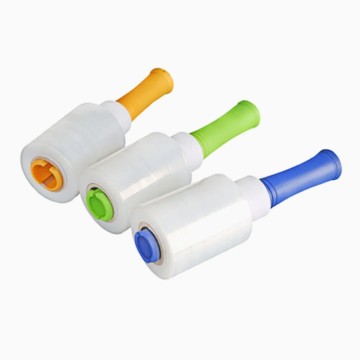
Our flagship PE cling film products are precision-engineered for the demanding requirements of food and beverage multipack bundling, offering outstanding transparency, puncture resistance, and reliable cling performance.
A deep dive into the technology, commercial landscape, and industrial applications driving global adoption.
Polyethylene (PE) cling film — also known as stretch wrap, shrink bundling film, or multipack overwrap — has become one of the most critical packaging materials in the global food and beverage supply chain. Specifically engineered for multipack applications, PE cling film holds together clusters of bottles, cans, cartons, pouches, and trays into a single retail-ready unit, enabling efficient logistics, shelf appeal, and consumer convenience simultaneously.
Unlike generic plastic wraps, PE cling film designed for food and beverage multipacks must satisfy a rigorous set of technical and regulatory requirements: food-contact safety certifications (FDA, EU 10/2011), precise cling-to-cling adhesion without adhesives, high optical clarity for barcode scanning and product visibility, and mechanical strength sufficient to withstand automated high-speed packaging lines running at 200–600 packs per minute.
The global stretch and cling film market was valued at over USD 12 billion in 2023 and is projected to exceed USD 18 billion by 2030, with food and beverage multipack applications accounting for more than 38% of total consumption volume — the single largest end-use segment.
The food and beverage industry represents the most demanding and highest-volume consumer of PE cling film worldwide. Major beverage producers — including carbonated soft drink, water, beer, and juice manufacturers — rely on PE shrink or stretch bundling film to replace traditional cardboard secondary packaging, reducing material cost by 30–55% per pallet while improving line speed and reducing carbon footprint per unit.
Globally, the shift from corrugated cardboard trays to full-wrap or pad-plus-film PE multipack configurations has accelerated dramatically since 2018. Retailers such as Walmart, Carrefour, and Tesco have actively encouraged this transition as part of their sustainability commitments, since PE multipack film uses up to 70% less material by weight compared to equivalent cardboard packaging.
In the food sector, PE cling film multipacks are extensively used for dairy products (yogurt pots, butter blocks, cheese portions), fresh produce (tomatoes, mushrooms, herbs), frozen foods, condiment bottles, and ready-meal trays. The film must maintain integrity across a wide temperature range — from cold-chain storage at -18°C to ambient retail environments — without losing cling strength or becoming brittle.
The PE cling film sector for food and beverage multipacks is undergoing rapid technological transformation. The following trends are reshaping product development and competitive positioning:
| Trend | Technology | Impact on Multipacks |
|---|---|---|
| Downgauging | Metallocene LLDPE, nano-layer coextrusion | Film thickness reduced from 50µm to 25–30µm with equivalent or superior mechanical properties; significant cost and material savings |
| Recyclability | Mono-material PE structures (all layers PE) | Enables closed-loop recycling via PE film streams; meets EU Packaging & Packaging Waste Regulation (PPWR) requirements |
| Bio-based PE | Sugarcane-derived ethylene polymerization | Drop-in replacement for fossil-based PE; reduces Scope 3 carbon emissions; supports brand ESG reporting |
| High-clarity optics | Biaxial orientation, anti-haze additives | Haze values below 3%; enhances product visibility and barcode readability at point of sale |
| Smart printing integration | Digital flexo, QR/NFC embeds | Enables track-and-trace, anti-counterfeiting, and consumer engagement directly on the multipack film |
| High-speed compatibility | Low-temperature shrink formulations | Shrink activation at 120–140°C reduces energy consumption in tunnel by 18–25% |
This is the highest-volume application for PE cling film in the food and beverage sector. Carbonated beverages, water, beer, and energy drinks are bundled using either full-shrink PE film (360° wrap with heat-shrink tunnel) or pad-plus-collar configurations. The film must deliver a tight, rattle-free bundle while allowing easy consumer separation. Typical specifications: 30–45µm thickness, 15–25% longitudinal pre-stretch, shrink force 2–4 N/15mm, haze
Yogurt pots, cream cheese tubs, butter blocks, and UHT milk cartons present unique challenges: irregular shapes, cold-chain exposure, and condensation. PE cling film for dairy multipacks requires excellent cold-temperature cling retention, anti-fog additives for retail display clarity, and compatibility with wet surfaces. Modified atmosphere retention is increasingly required for premium dairy lines.
Tomatoes-on-the-vine, herb bunches, mushroom punnets, and citrus clusters are increasingly presented in PE film multipacks rather than foam netting or cardboard trays. The film must be breathable (micro-perforated) to prevent condensation and ethylene buildup, while maintaining structural integrity through cold-chain logistics. Compostable and bio-based PE variants are gaining traction in this segment.
Premium beer, wine, and spirits producers use PE shrink film multipacks as a cost-effective alternative to cardboard carriers. The film must withstand the significant weight of glass bottles (often 3–5 kg per multipack), requiring high puncture resistance (>400 g/25µm) and anti-slip surface treatment to prevent stack collapse during palletization and transport.
Convenience food manufacturers bundle tray-based products into 2-pack, 3-pack, or promotional multipacks using PE cling film. These applications demand excellent seal integrity at low temperatures, resistance to food oils and sauces, and compatibility with high-speed tray-wrapping equipment. Printed PE film with promotional messaging is standard in this segment.
Beyond retail multipacks, PE stretch film plays a critical role in secondary and tertiary packaging — unitizing finished multipack cases on pallets for warehouse storage and international shipping. LLDPE pallet wrap film with 150–300% pre-stretch capability reduces film consumption per pallet by 40–60% compared to standard PE, while delivering superior load containment force.
Leading PE cling film manufacturers are investing heavily in PCR (post-consumer recycled) content integration — achieving up to 30% rPE content without compromising food-contact compliance or mechanical performance. Closed-loop collection programs, in-store film recycling bins, and chemical recycling partnerships are creating viable end-of-life pathways that position PE multipack film as a genuinely circular packaging solution.
Choosing the optimal PE cling film specification requires evaluation across multiple performance dimensions. Below are the critical parameters that procurement and packaging engineers must assess:
Range: 15–80µm. Thinner gauges (15–30µm) for lightweight beverage bundles; heavier gauges (50–80µm) for glass bottle and heavy-load applications. Precision gauge control (±2%) ensures consistent machine performance.
Minimum tensile strength 28 MPa (MD/TD). Puncture resistance critical for sharp-edged cans and bottle caps. Elmendorf tear resistance ensures bundle integrity under dynamic handling stresses.
Haze below 5% for retail applications; below 3% for premium products. High gloss (>80 GU) enhances shelf presence. Anti-fog treatment essential for refrigerated display environments.
Shrink onset temperature 100–160°C depending on formulation. Free shrink 40–70% at 120°C for full-wrap configurations. Low-energy shrink formulations reduce tunnel operating costs by up to 25%.
Full compliance with FDA 21 CFR, EU Regulation 10/2011, and China GB standards. Migration testing for all additives. REACH and RoHS compliance for export markets. Available with Halal and Kosher certification on request.
Engineered for compatibility with leading OEM shrink-wrap systems (Kallfass, Cermex, Lantech, Robopac). Consistent COF (coefficient of friction) ensures smooth film feed at line speeds up to 600 packs/min without jams or misfeeds.
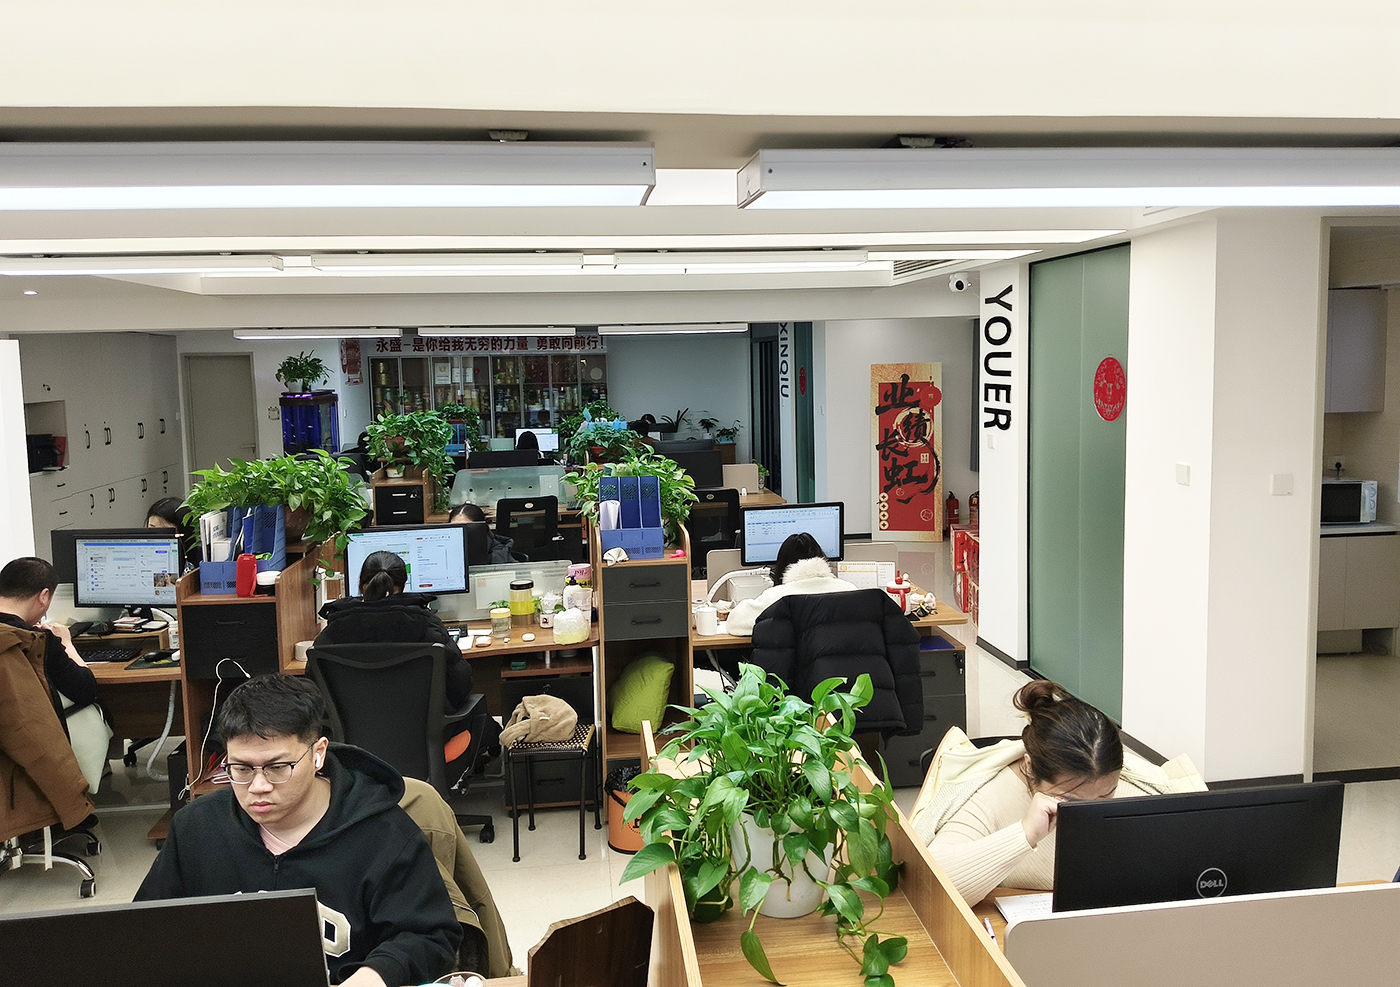
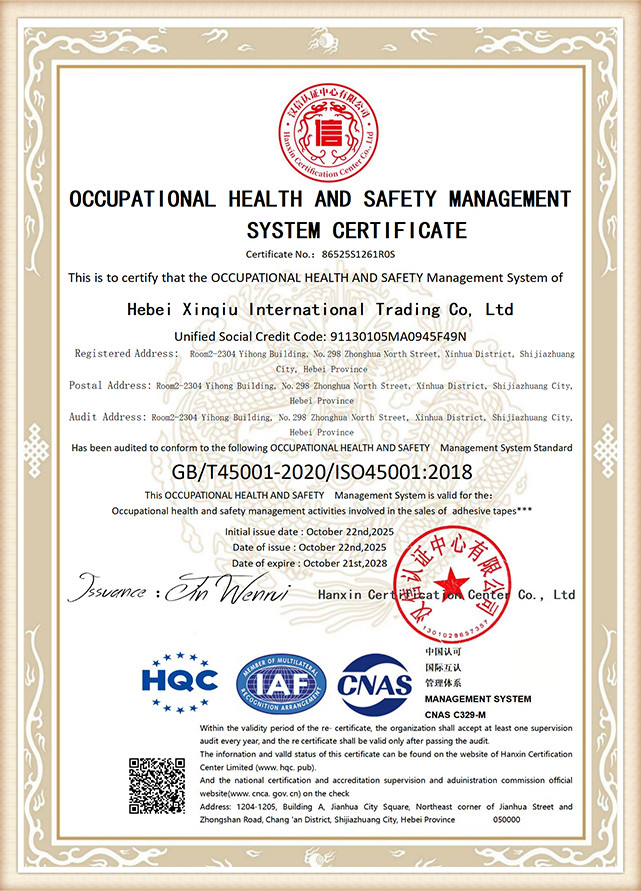
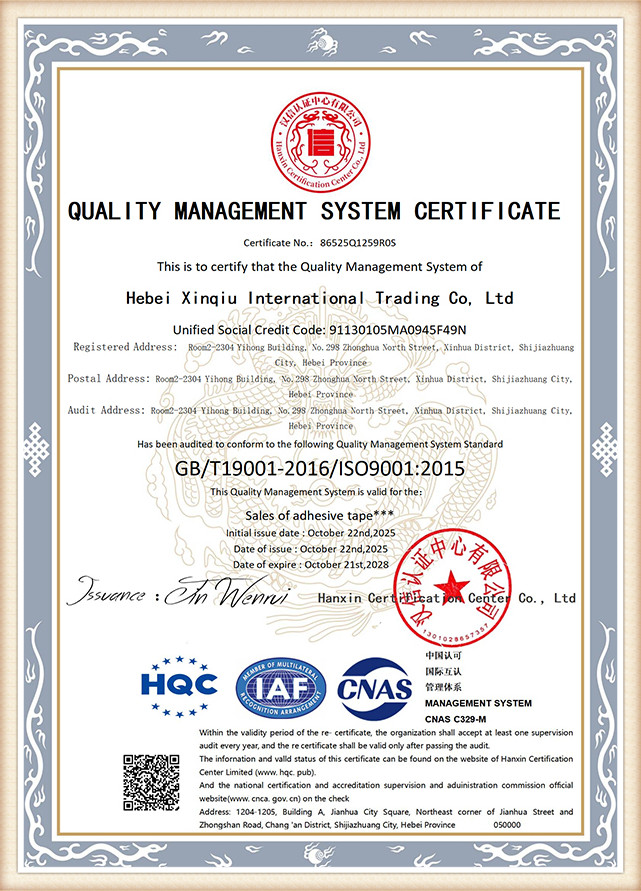
Hebei Youer New Material Science and Technology Co., Ltd. has been founded since 2007. It is located in Shijiazhuang City, Hebei Province, and has specialized in film for more than 10 years and becomes a modern high-tech enterprises integrating R & D, production and sales.
Our product system focuses on three core product lines — stretch film, protective film and BOPP film, with detailed extended classifications to fully cover the diverse application needs of various industries.
With experience in product development and materials exporting, we have gained a very good reputation among customers from more than 80 countries. Our professional sales team which is always ready to give quick response, provide multi choice to satisfy customer requirements with one stop service.
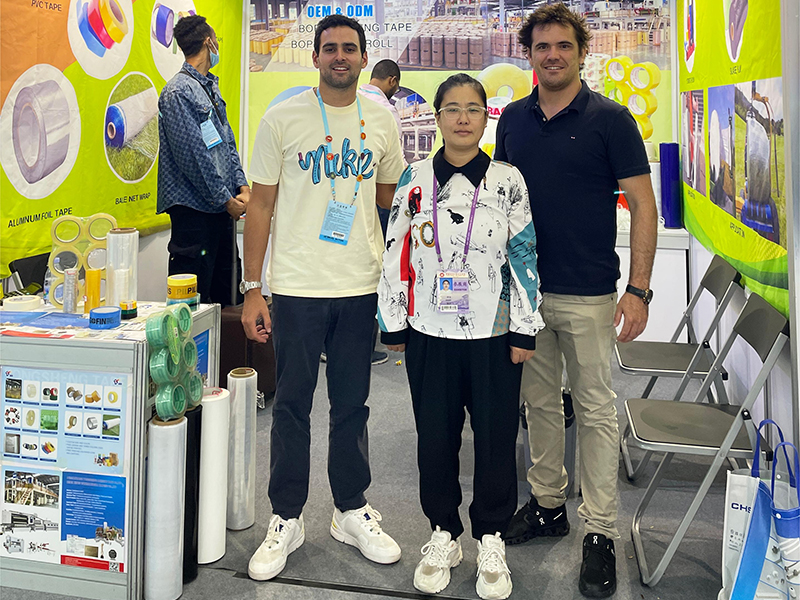
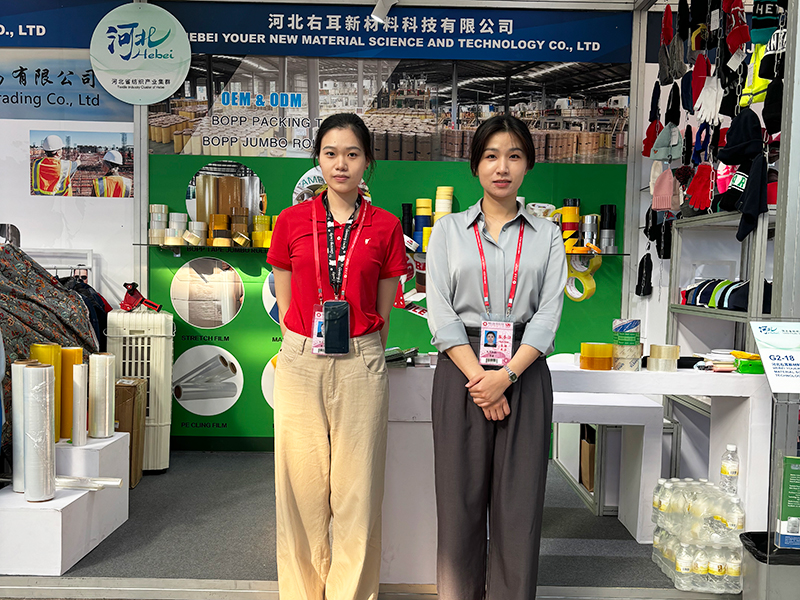
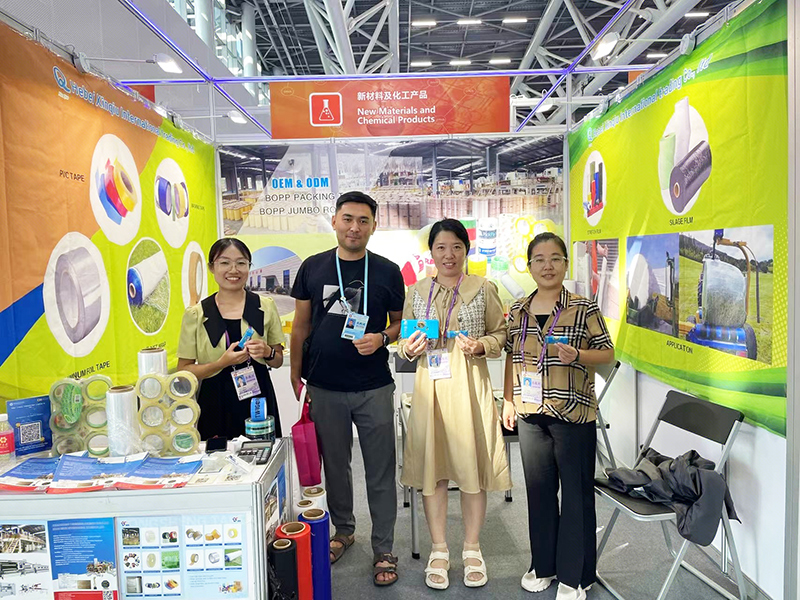
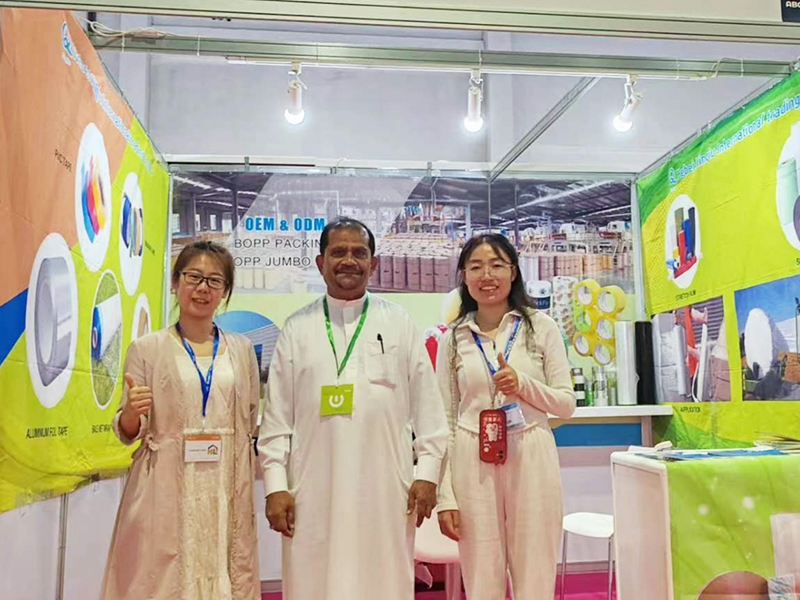
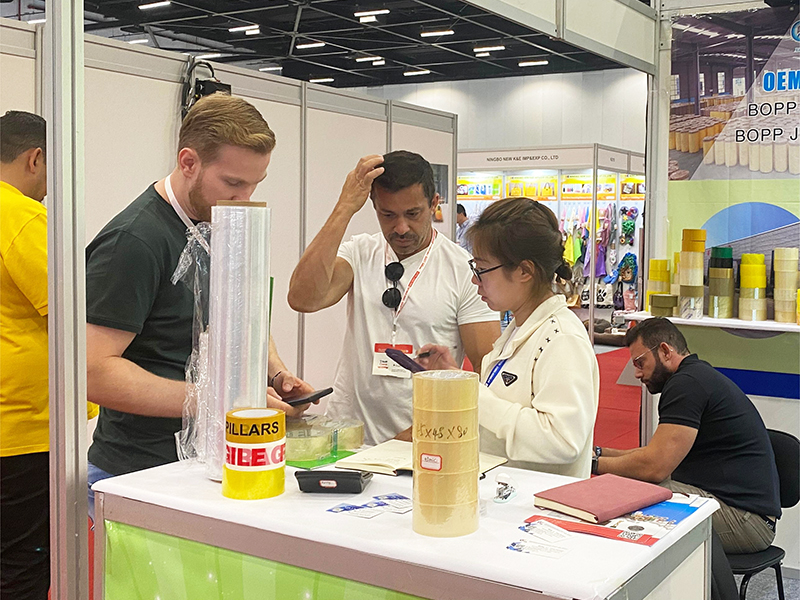
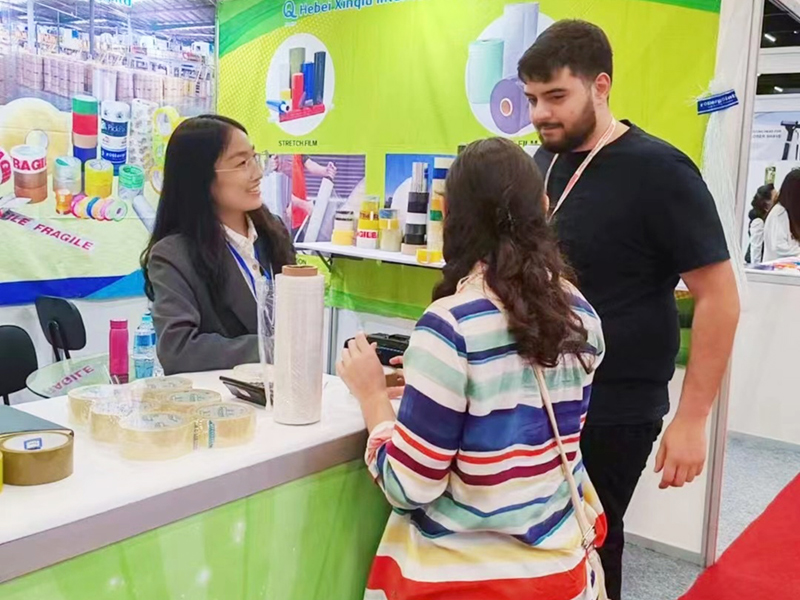
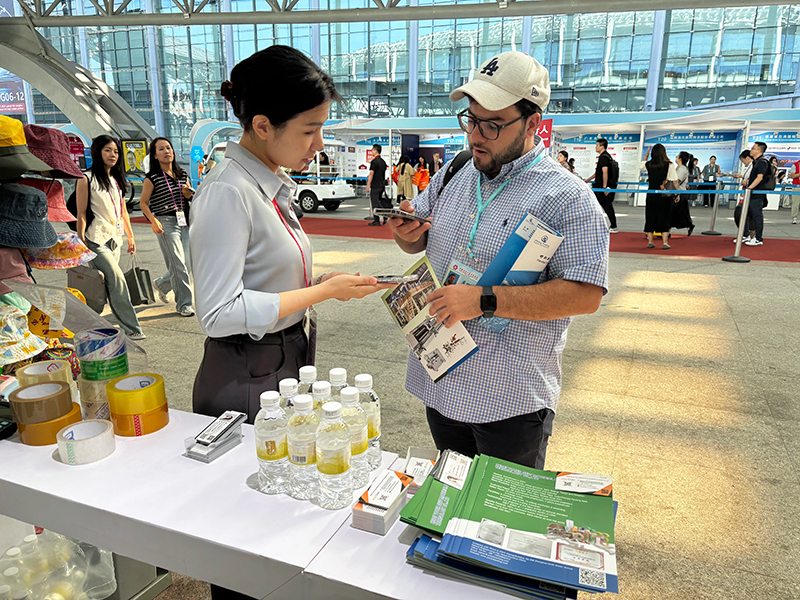
Youer Films actively participates in international packaging and materials trade exhibitions, showcasing our latest PE cling film innovations for food and beverage multipack applications to global buyers and partners.
Explore our full range of PE and protective film solutions — all engineered to meet the precision demands of food, beverage, and industrial multipack applications worldwide.