- admin@youerfilms.com
- Mon - Sat at 9:00AM to 18:00PM
Leave Your Message
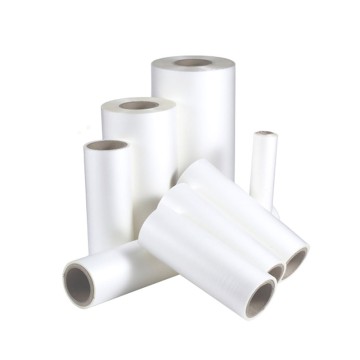
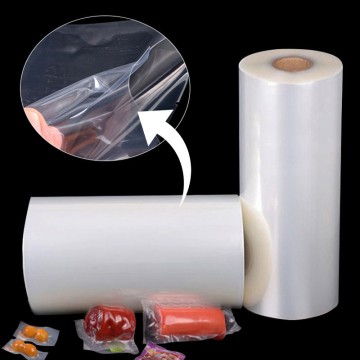
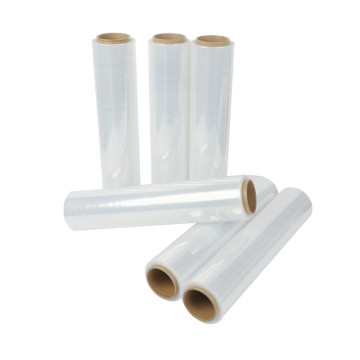
Engineered packaging films specifically designed for food and beverage collation, ensuring structural integrity and shelf appeal.
The global packaging industry has witnessed a monumental shift in how products are bundled, shipped, and displayed. Packaging Film For Food And Beverage Multipacks is no longer just a protective layer; it is a highly engineered, AI-optimized material crucial for modern commerce. In today's fast-paced retail environments, secondary packaging must fulfill multiple roles simultaneously: ensuring load stability during rigorous transit, providing pristine optical clarity for brand visibility, and meeting stringent environmental regulations.
Industrially, the demand for collation shrink films and stretch wraps has surged due to the rise of club stores, bulk purchasing trends, and e-commerce logistics. Manufacturers are transitioning away from traditional, heavy corrugated cardboard boxes to lightweight, high-tensile polymer films. This transition significantly reduces the overall carbon footprint, lowers freight costs by decreasing pallet weight, and enhances the unboxing or un-shelving experience for both retailers and end-consumers. State-of-the-art production lines now utilize smart sensors and AI-driven quality control to ensure that every micron of the film offers maximum puncture resistance and optimal shrinkage ratios.
Commercially, the visual appeal of a multipack can make or break a sale at the point of purchase. High-grade BOPP and advanced PE blends offer exceptional printability. This allows beverage brands to transform a simple bundle of water bottles or energy drinks into a vibrant, 360-degree advertising billboard. The integration of anti-fog properties and high-gloss finishes ensures that products stored in refrigerated aisles remain highly visible and attractive, directly influencing consumer buying behavior and driving revenue growth for FMCG (Fast-Moving Consumer Goods) brands.
The versatility of Packaging Film For Food And Beverage Multipacks allows it to be perfectly tailored to highly specific industrial applications. Understanding the nuanced requirements of different product categories is essential for selecting the optimal polymer blend and film structure.
For high-speed canning and bottling lines, collation shrink film is the industry standard. The film must exhibit rapid and uniform shrinkage when passing through heat tunnels, creating a tight "bullseye" closure at the ends. This ensures the multipack remains rigid, preventing individual cans or bottles from shifting, which is critical for pallet stability and preventing scuffing during transit.
Dairy products and liquid foods packaged in aseptic cartons require secondary films that offer gentle yet firm containment. Excessive tension can crush the delicate primary packaging, while too little leads to loose bundles. Specialized low-temperature shrink films are deployed here, ensuring the structural integrity of the cartons while maintaining the cold-chain efficiency required for perishable goods.
Snack multipacks often utilize advanced BOPP (Biaxially Oriented Polypropylene) films. These films provide an excellent moisture and oxygen barrier, extending the shelf life of the enclosed products. Furthermore, the use of matte or metallized finishes on these films imparts a premium tactile and visual aesthetic, crucial for brand positioning in highly competitive retail snack aisles.
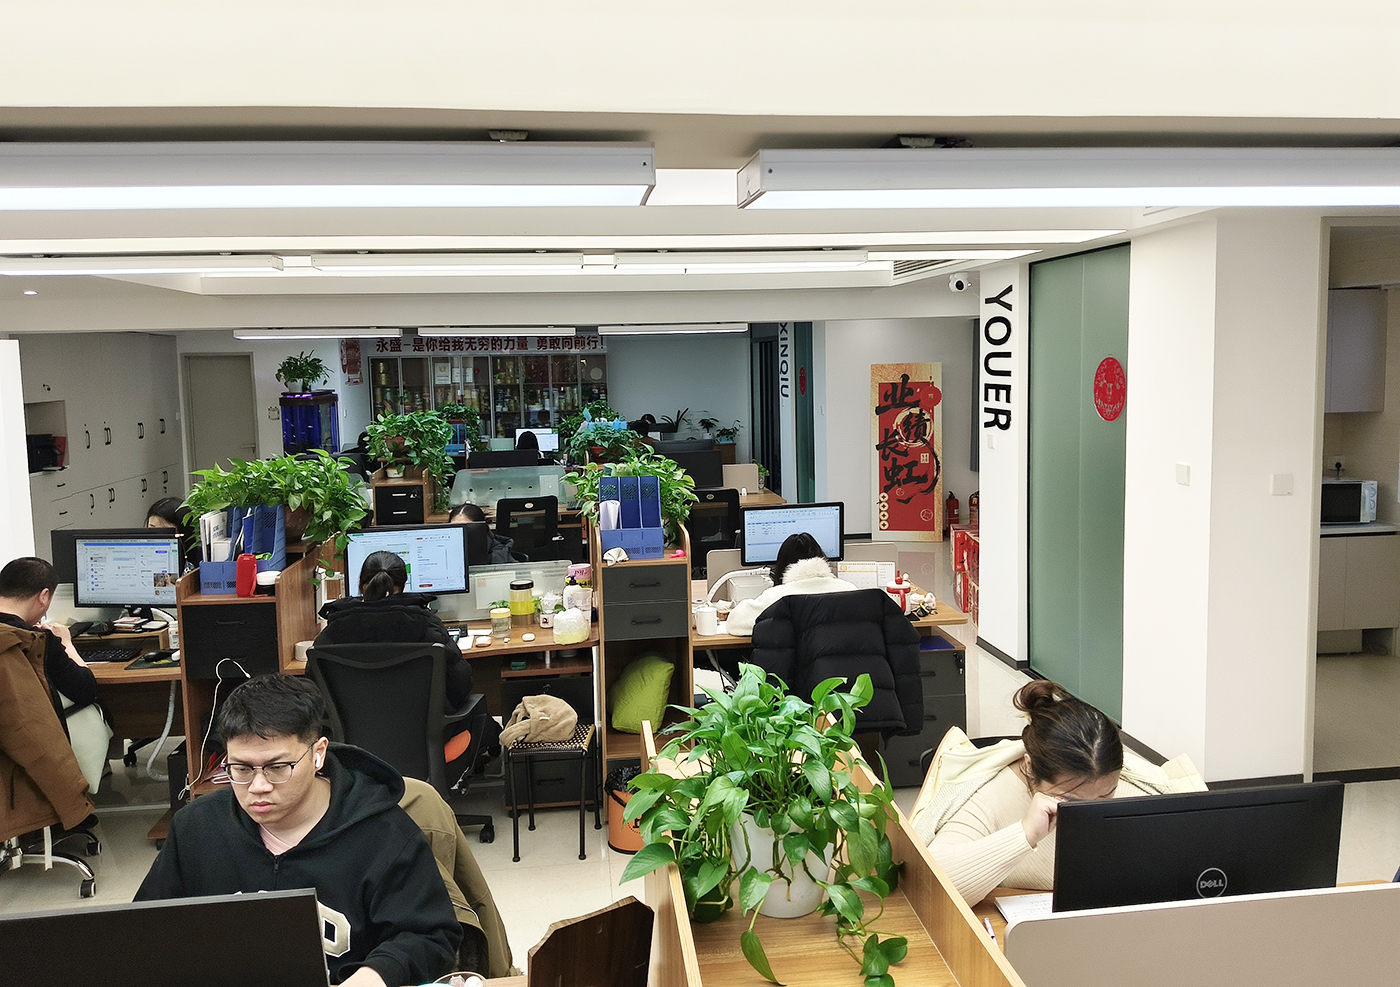
Hebei Youer New Material Science and Technology Co., Ltd. has been founded since 2007. It is located in Shijiazhuang City, Hebei Province, and has specialized in film for more than 10 years and becomes a modern high-tech enterprises integrating R & D, production and sales.
Our product system focuses on three core product lines — stretch film, protective film and BOPP film, with detailed extended classifications to fully cover the diverse application needs of various industries.
With experience in product development and materials exporting, we have gained a very good reputation among customers from more than 80 countries. Our professional sales team which is always ready to give quick response, provide multi choice to satisfy customer requirements with one stop service.
The landscape of Packaging Film For Food And Beverage Multipacks is undergoing a rapid technological revolution, heavily influenced by global sustainability mandates and the integration of Artificial Intelligence in manufacturing processes. As we look to the future, several key trends are redefining how packaging films are engineered, produced, and recycled.
1. Extreme Downgauging and High-Performance Resins: Driven by the need to reduce plastic usage without compromising strength, the industry is embracing extreme downgauging. By utilizing advanced metallocene polyethylenes and multi-layer co-extrusion technologies (often up to 7 or 9 layers), manufacturers can produce films that are up to 30% thinner than legacy products. These micro-thin films maintain exceptional holding force, tear resistance, and optical clarity, drastically reducing the volume of material entering the waste stream.
2. Sustainable and Biodegradable Innovations: The push towards a circular economy is accelerating the adoption of Post-Consumer Recycled (PCR) resins and bio-based polymers like PLA (Polylactic Acid). Modern food-grade cling films and stretch rolls are increasingly formulated to be fully biodegradable or compostable. This shift not only aligns with international environmental regulations but also resonates deeply with eco-conscious consumers who actively seek out brands committed to reducing ocean plastics and landfill waste.
3. AI-Driven Smart Manufacturing: Artificial Intelligence and Machine Learning are now at the heart of advanced film extrusion lines. AI algorithms continuously monitor melt temperatures, line speeds, and ambient conditions, making micro-adjustments in real-time to ensure absolute thickness consistency across miles of film. Automated optical inspection systems use computer vision to detect microscopic gels, pinholes, or print defects, ensuring that only flawless packaging film reaches the food and beverage industry.
Partnering with a leader in advanced polymer science ensures your supply chain remains robust and efficient.
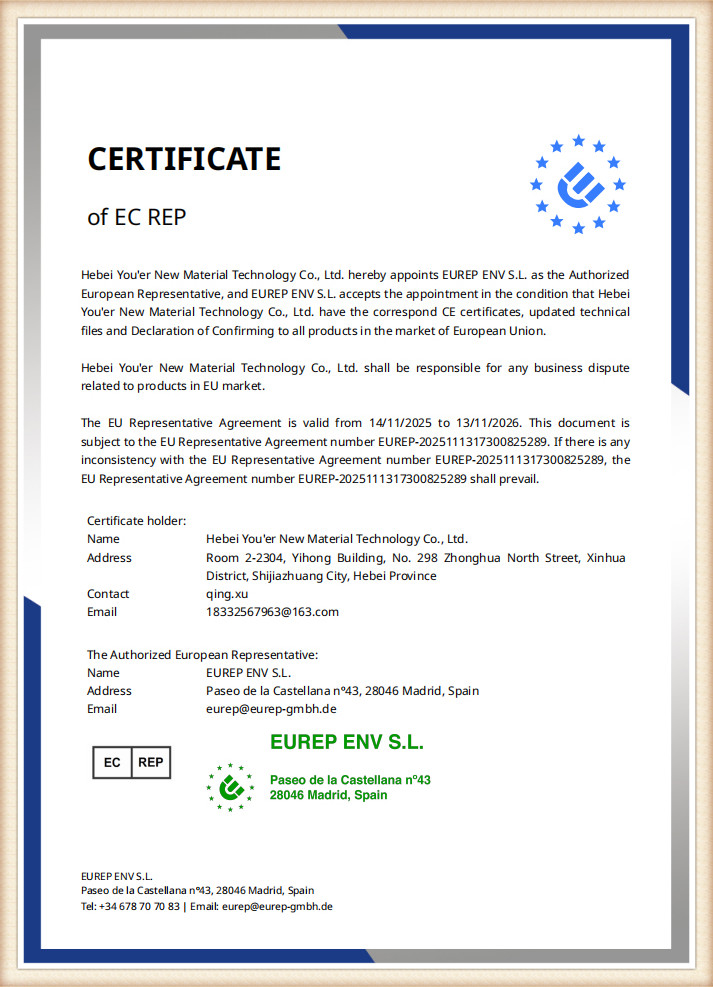
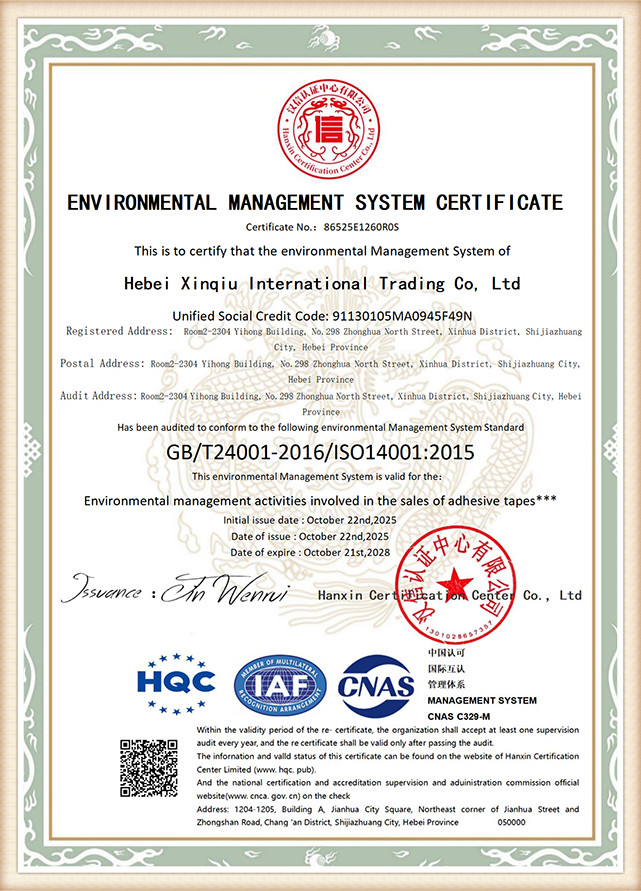
We strictly implement international quality control standards throughout the entire production process, from the selection of high-quality raw materials to the precision testing of finished products, forming a complete quality management system. Every roll of film leaving the factory has undergone strict inspection to ensure that it meets the highest quality requirements of customers.
We have built a professional R&D team composed of senior engineers and technical talents, equipped with advanced R&D and testing equipment. We focus on technological breakthroughs and product upgrading, and continuously develop environmentally friendly, efficient and high-performance film products to keep pace with the changing market demand and lead the industry development trend.
Our vision is to become a world-class film manufacturer, promote the sustainable development of the film industry, and create greater value for customers, employees and society through continuous innovation and unremitting efforts. We are looking forward to build up a long term partnership with more and more potential customers all over the world.
Integrating high-quality Packaging Film For Food And Beverage Multipacks into a company's operations yields profound economic benefits that ripple throughout the entire supply chain. It is a strategic investment that optimizes logistics, reduces product damage, and enhances overall operational profitability.
From a logistics standpoint, the transition from rigid packaging to flexible film multipacks dramatically improves pallet density. Because film conforms tightly to the contours of the products, dead space is minimized. This allows more units to be loaded onto a single pallet, and consequently, more pallets into a shipping container or truck. The resulting reduction in freight costs and fuel consumption is substantial, directly improving the bottom line while simultaneously lowering the corporate carbon footprint.
Furthermore, the superior puncture resistance and load retention capabilities of advanced stretch and shrink films drastically reduce the incidence of product damage during transit. In the food and beverage sector, a broken seal or dented can often leads to the rejection of an entire case. By ensuring that multipacks arrive at distribution centers and retail shelves in pristine condition, companies minimize shrinkage, reduce costly returns, and protect their brand equity in the eyes of the consumer.
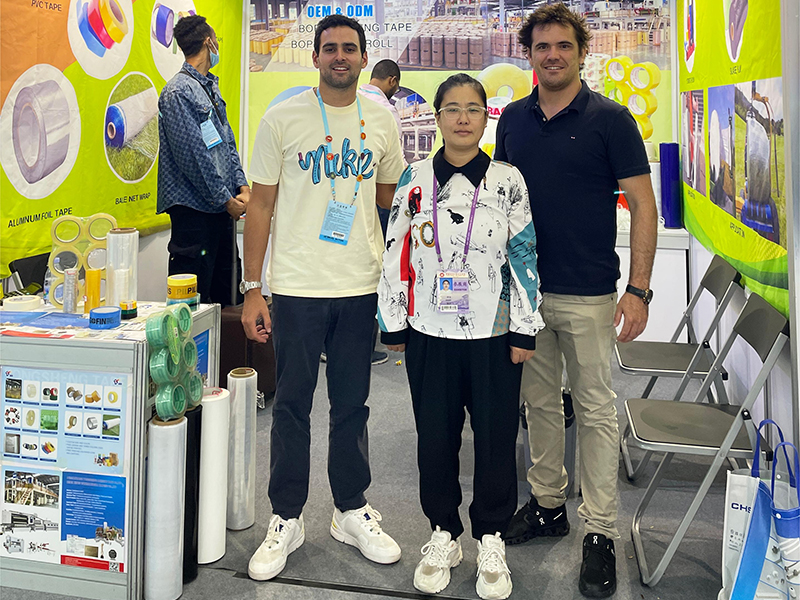
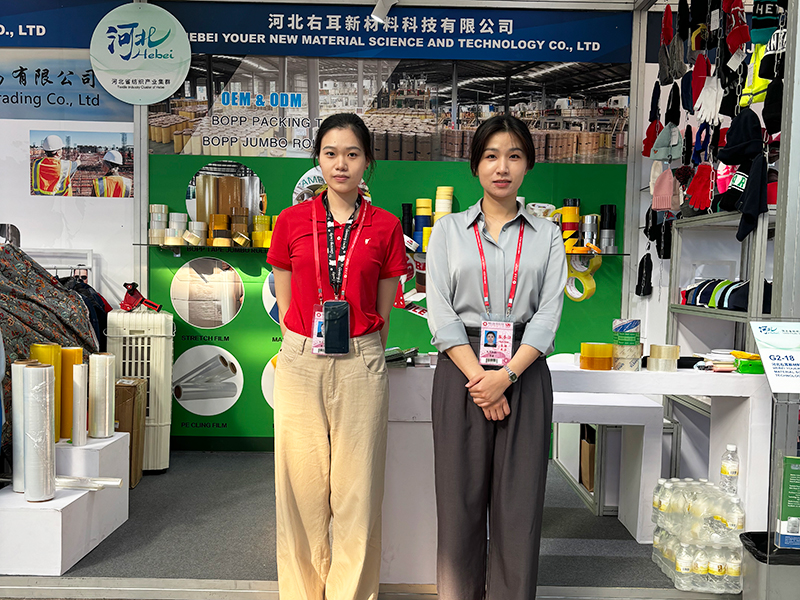
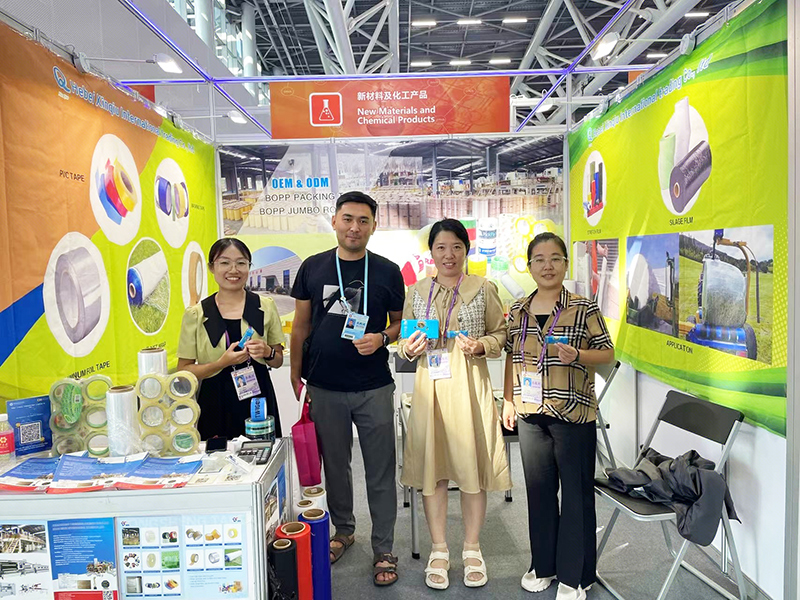
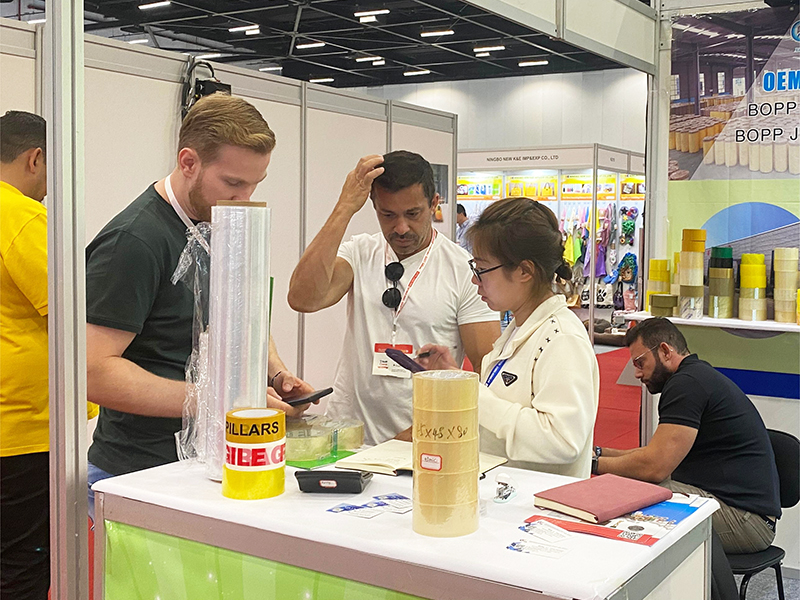
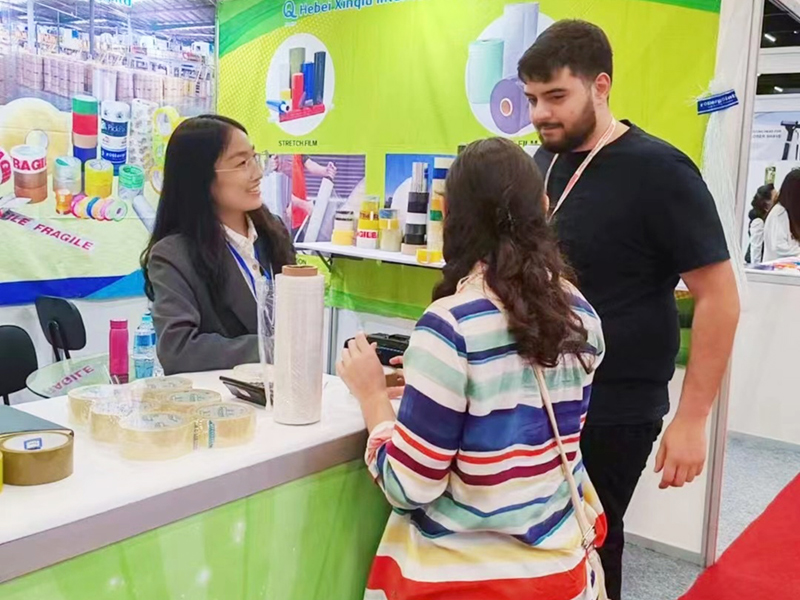
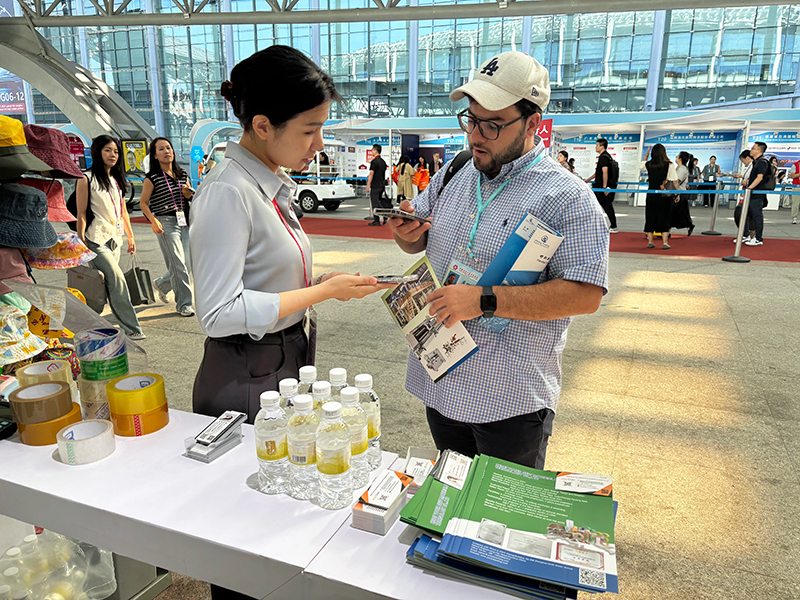
A testament to our global presence and commitment to excellence in the packaging film industry.
Explore our full range of high-performance films engineered for diverse industrial and commercial applications.