- admin@youerfilms.com
- Mon - Sat at 9:00AM to 18:00PM
Leave Your Message
Industry-leading packaging film solutions trusted by global manufacturers and logistics partners
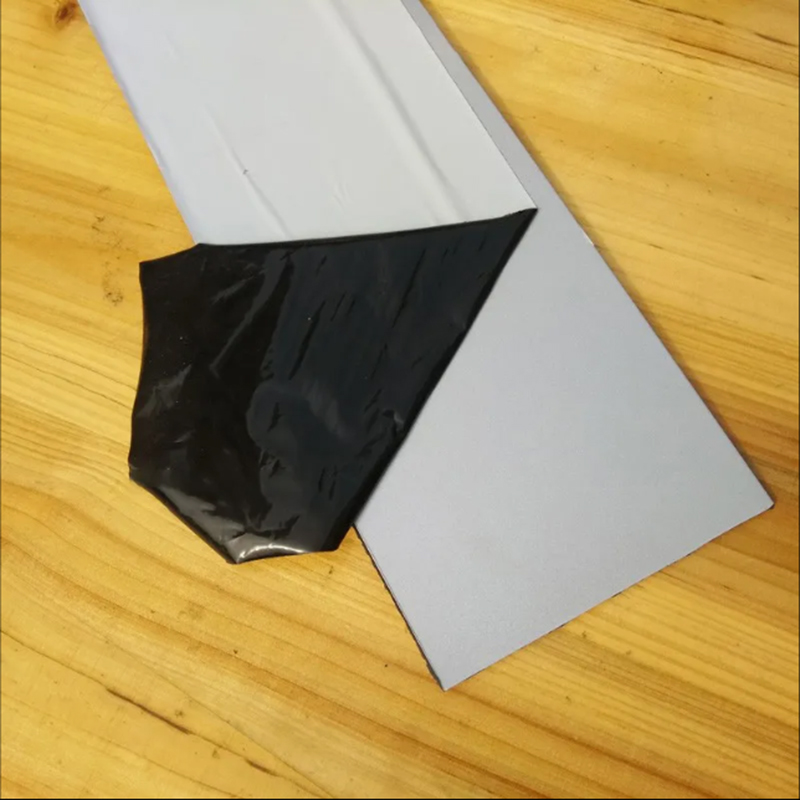
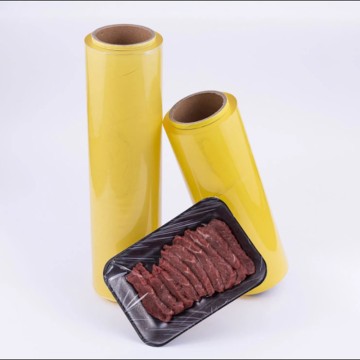
High-Density Polyethylene (HDPE) film has emerged as one of the most critical materials in modern industrial packaging, specifically engineered to meet the demanding requirements of pallet wrapping and long-distance shipping. As global trade volumes expand and supply chain complexity grows, HDPE film stands at the forefront of packaging innovation — offering an unmatched combination of mechanical strength, chemical resistance, moisture barrier properties, and cost efficiency.
Unlike standard polyethylene films, HDPE film is produced through a controlled polymerization process that results in a highly crystalline, dense molecular structure. This gives HDPE film its signature toughness, stiffness, and resistance to puncture and tearing — properties that are absolutely essential when securing palletized loads for transit across warehouses, ports, rail networks, and international shipping routes.
HDPE film is now used across more than 80+ countries as the preferred material for industrial pallet wrapping, replacing traditional rope, metal strapping, and low-grade PE films in high-value and heavy-duty logistics applications.
The global stretch and pallet wrap film market — of which HDPE film is a significant segment — is valued at over USD 8 billion and growing steadily at 4–6% CAGR. This growth is being driven by several powerful forces in manufacturing, e-commerce, food & beverage, construction, and pharmaceutical logistics sectors.
From automated stretch-wrapping machines in Amazon fulfillment centers to manual hand-wrap applications in small export workshops across Southeast Asia, HDPE pallet film is proving indispensable. Major economies — including the United States, Germany, Japan, South Korea, Australia, and the Middle East — are increasing their procurement volumes annually, largely sourcing from high-quality Chinese film manufacturers who have invested heavily in precision blown-film and cast-film extrusion lines.
In the industrial supply chain, HDPE film functions as more than just a wrap — it is a critical containment system. A properly wrapped pallet using HDPE film can withstand compressive forces exceeding 1,500 kg, vibration from freight transport, humidity changes during container shipping, and even minor impacts during loading and unloading. This performance profile makes HDPE film the material of choice for industries where product loss during transit equates to serious financial and reputational damage.
Engineered for performance — designed for the real world of industrial shipping and logistics
HDPE film's high tensile strength and elongation recovery ensure palletized goods remain tightly secured during multi-modal transport — truck, ship, rail, or air freight.
The dense molecular structure of HDPE creates an effective vapor and moisture barrier, protecting packaged goods from humidity-related damage during container transit and outdoor storage.
HDPE film resists puncture from sharp pallet edges, staples, or warehouse handling equipment — critical for reducing film breakage during automated wrapping cycles.
HDPE is widely accepted in global plastics recycling streams. Brands transitioning to circular economy packaging models favor HDPE for its recyclability credentials and lower carbon footprint versus multi-layer composites.
Performing reliably from −40°C to +80°C, HDPE film maintains integrity during cold chain logistics, frozen food shipping, and high-heat warehouse environments near loading docks.
Available in pre-stretch formulations for turntable wrapping machines and hand-roll formats for manual application — HDPE film adapts to every scale of packing operation.
From cold chain to hazardous freight — HDPE film serves every sector of the global supply chain
HDPE film is extensively used to wrap pallets of bottled beverages, canned goods, frozen meat, and dairy products. Its food-safe, non-toxic composition complies with FDA and EU food contact material standards. In cold chain logistics, HDPE film maintains its cling and barrier properties at sub-zero temperatures, making it the preferred choice for cold storage distribution centers worldwide.
Bricks, tiles, insulation boards, PVC pipes, and steel rods are routinely palletized and secured with heavy-gauge HDPE film before shipping to construction sites globally. HDPE's superior UV stabilization options allow wrapped pallets to remain outdoors for extended periods without film degradation, preventing moisture ingress and protecting expensive building materials.
High-value electronics shipments require anti-static and ESD-compliant HDPE film to prevent electrostatic discharge damage during pallet wrapping. Television sets, washing machine units, and server rack equipment manufacturers rely on precision-formulated HDPE film as the outer containment layer before final export container loading.
Pharmaceutical pallet wrapping demands film that maintains strict hygiene, prevents contamination, and provides tamper-evidence. HDPE film with colored tinting or printed security markings is increasingly used by pharma distributors to ensure shipment integrity from factory to hospital warehouse — complying with GDP (Good Distribution Practice) guidelines.
HDPE's excellent chemical resistance makes it ideal for wrapping palletized drums of industrial chemicals, lubricants, and cleaning agents. HDPE film does not react with common chemicals and creates a secondary containment barrier that reduces risk of contamination or spillage during shipping and storage.
Precision-machined automotive components, bearings, gearboxes, and stamped metal parts are palletized and wrapped with HDPE film to prevent surface corrosion, dust accumulation, and mechanical damage during long-distance OEM supply chain deliveries. Anti-corrosion VCI (Vapor Corrosion Inhibitor) HDPE films are a growing niche in this segment.
The explosive growth of e-commerce — now exceeding USD 6 trillion in global transaction value — has fundamentally transformed pallet wrapping requirements. Fulfillment centers operated by major retailers process thousands of pallets per day, each requiring consistent, machine-compatible HDPE film that can be applied at speeds of 25–40 pallets per hour without breakage or rewrapping.
HDPE pre-stretch film has become particularly popular in automated fulfillment environments, as it allows a single roll to wrap significantly more pallets than conventional film — reducing material cost by 30–50% and lowering per-pallet packaging labor costs. Smart logistics operators are pairing HDPE film with barcode and RFID tracking systems printed or embedded within film layers, enabling full pallet-level visibility throughout the shipping journey.
Industry Insight: Leading third-party logistics (3PL) providers report that switching to high-performance HDPE pre-stretch film reduces annual film consumption by an average of 35% while maintaining equivalent or superior load containment performance compared to standard LLDPE stretch film.
Key forces transforming how HDPE film is manufactured, used, and recycled globally through 2030
Nanocomposite additives — including nanoclay and graphene-based compounds — are being integrated into HDPE film formulations to achieve 40–60% improvement in tensile and barrier properties without increasing film thickness or material cost. This allows manufacturers to produce thinner, lighter films with superior performance.
Major FMCG and logistics brands have committed to incorporating 30–50% post-consumer recycled HDPE content in pallet films by 2027. Advanced decontamination and sorting technologies are making food-grade rHDPE commercially viable, and certification schemes such as APR (Association of Plastic Recyclers) are defining quality standards for recycled pallet film.
Embedded NFC chips and printed QR codes within HDPE film layers are enabling pallet-level tracking, temperature logging, and tamper detection throughout the supply chain. This convergence of packaging materials and digital technology represents a USD 1.2 billion market opportunity by 2028.
Bio-based polyethylene — derived from sugarcane ethanol and other renewable sources — is commercially available and chemically identical to fossil-based HDPE. Film manufacturers are blending bio-HDPE into pallet film formulations to reduce Scope 3 carbon emissions and satisfy ESG reporting requirements from multinational clients.
New-generation robotic pallet wrappers operating at 60+ pallets/hour demand HDPE film with extremely consistent gauge, high elongation-at-break values, and predictable pre-stretch behavior. Film manufacturers are investing in multi-layer co-extrusion technologies to produce machine-optimized HDPE film grades that eliminate downtime and film waste in automated packaging lines.
Southeast Asia, Africa, and Latin America are rapidly industrializing, creating enormous demand for cost-effective pallet wrapping solutions tailored to local climate and logistics infrastructure. Anti-UV HDPE films designed for tropical outdoor storage and high-slip formulations for humid warehouse conditions are seeing double-digit growth in these high-potential markets.
17+ years of film manufacturing expertise — serving 80+ countries with precision-engineered packaging materials
Powering reliable HDPE film supply for pallet wrapping across every continent
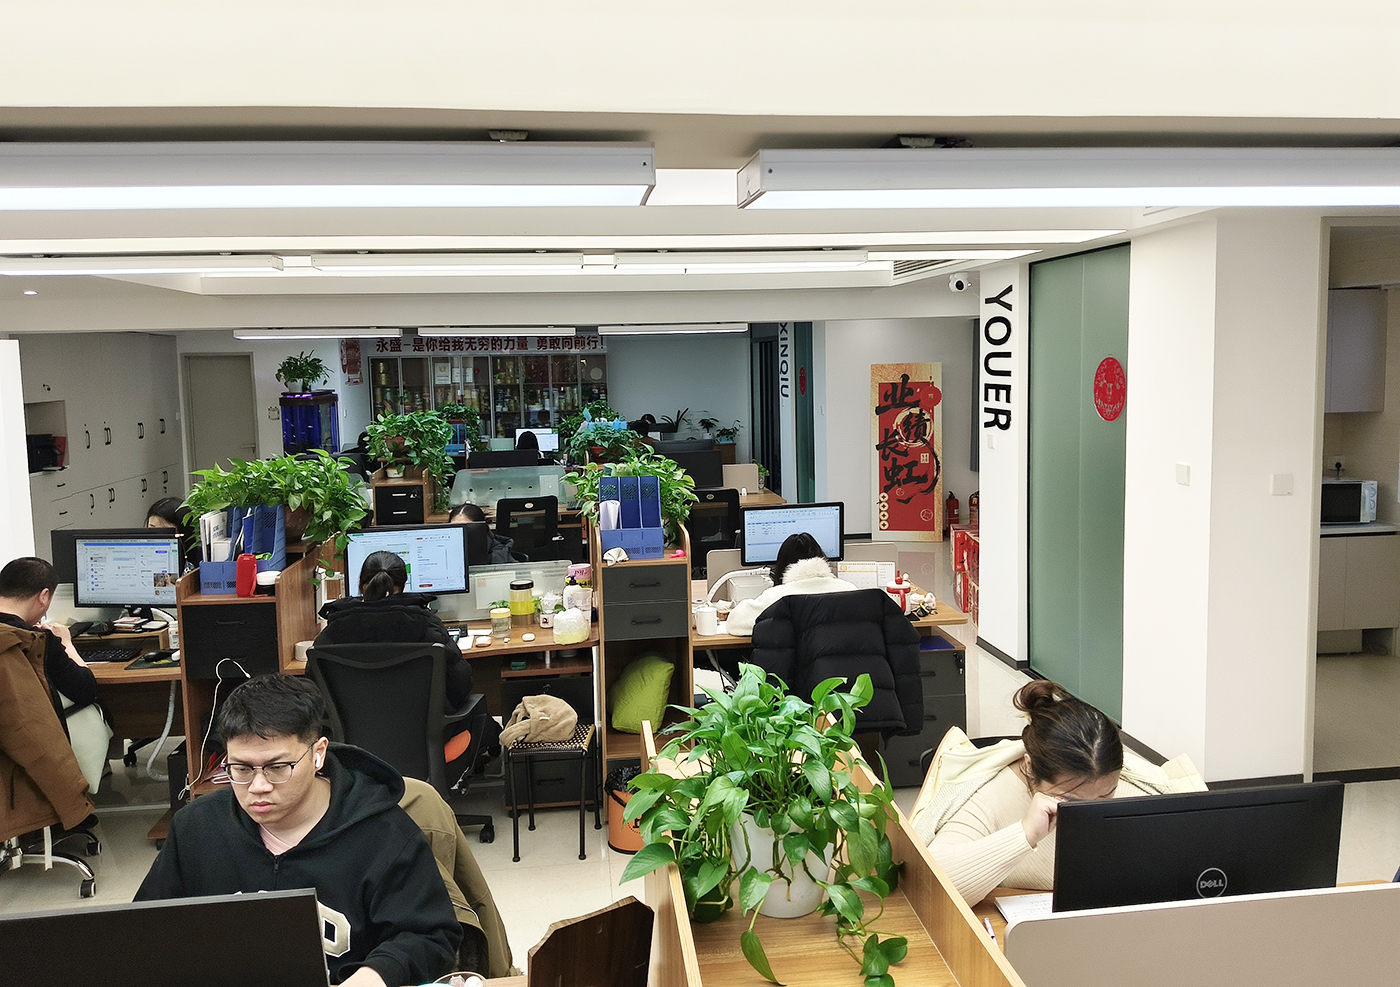
Founded in 2007 and headquartered in Shijiazhuang City, Hebei Province, China, Hebei Youer New Material Science and Technology Co., Ltd. has specialized in high-performance plastic film manufacturing for more than 17 years — growing into a modern high-tech enterprise integrating R&D, production, and sales under one roof.
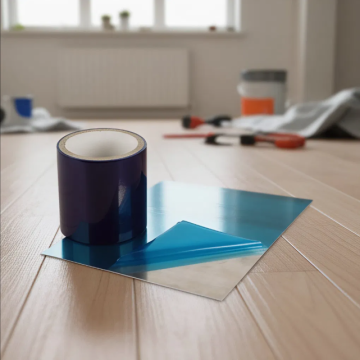
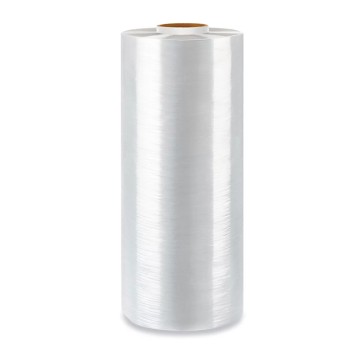
Our product system focuses on three core product lines — stretch film, protective film, and BOPP film — with detailed extended classifications to fully cover the diverse application needs of various industries. Our HDPE and LDPE pallet wrapping films are engineered to international performance standards and customized to meet the specific weight, size, color, and mechanical requirements of our clients across six continents.
With deep experience in product development and global materials exporting, we have earned an outstanding reputation among customers in more than 80 countries. Our professional, multilingual sales team is always ready with quick responses, multiple product options, and comprehensive one-stop packaging service to help your business ship smarter, safer, and more sustainably.
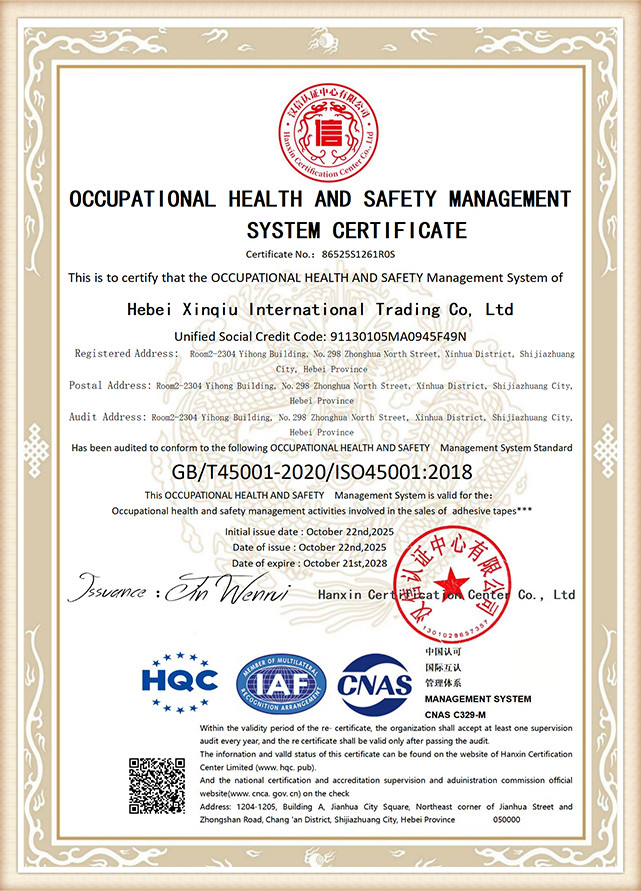
Internationally recognized standards backing every roll of HDPE pallet film we manufacture
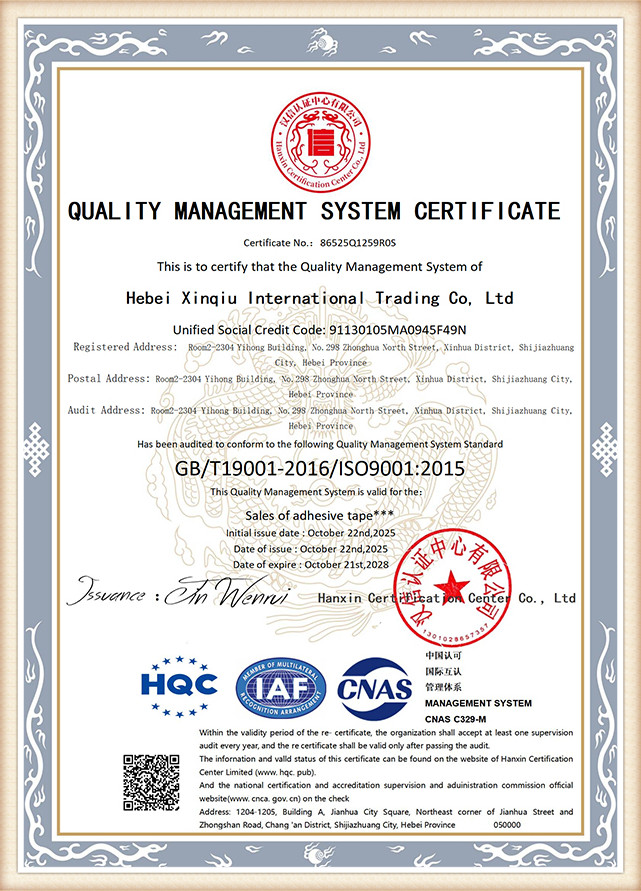
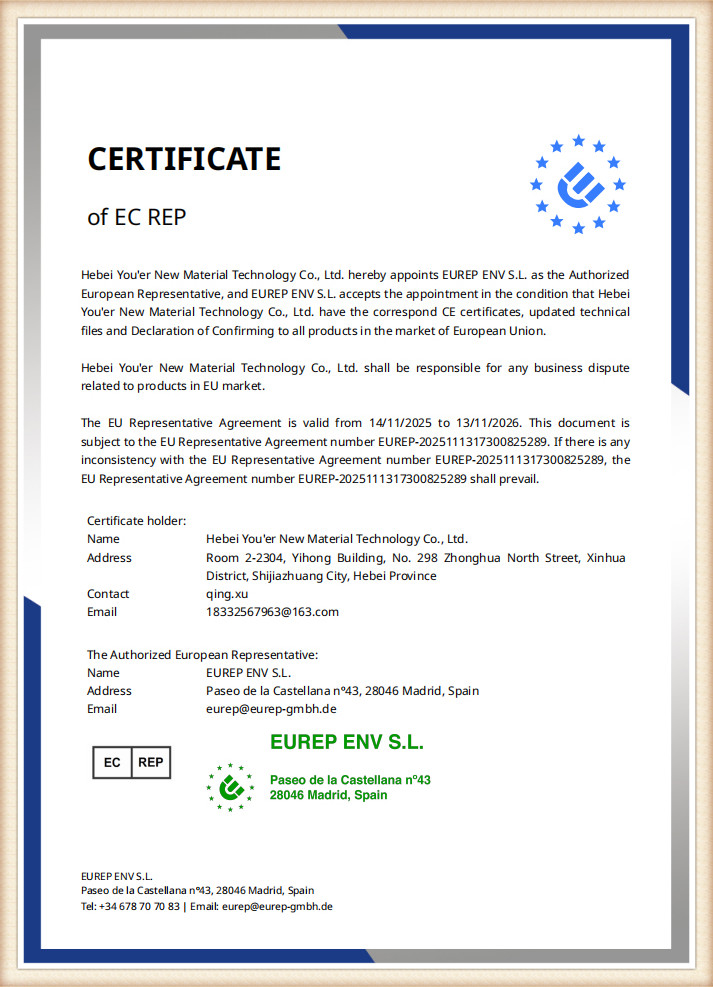
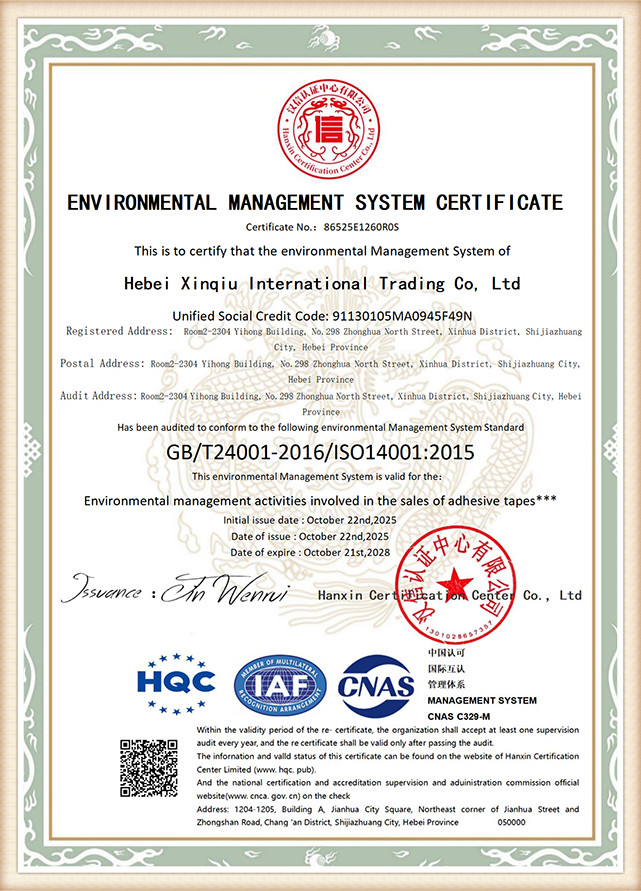
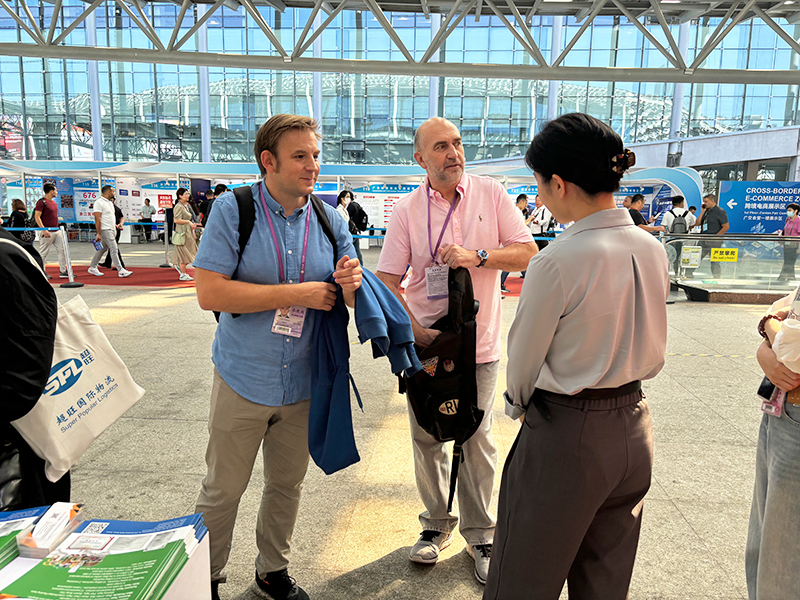
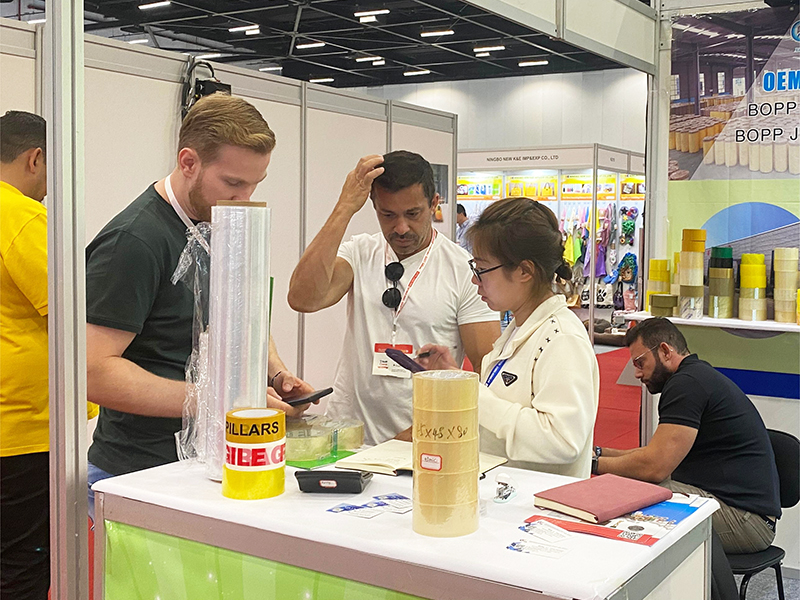
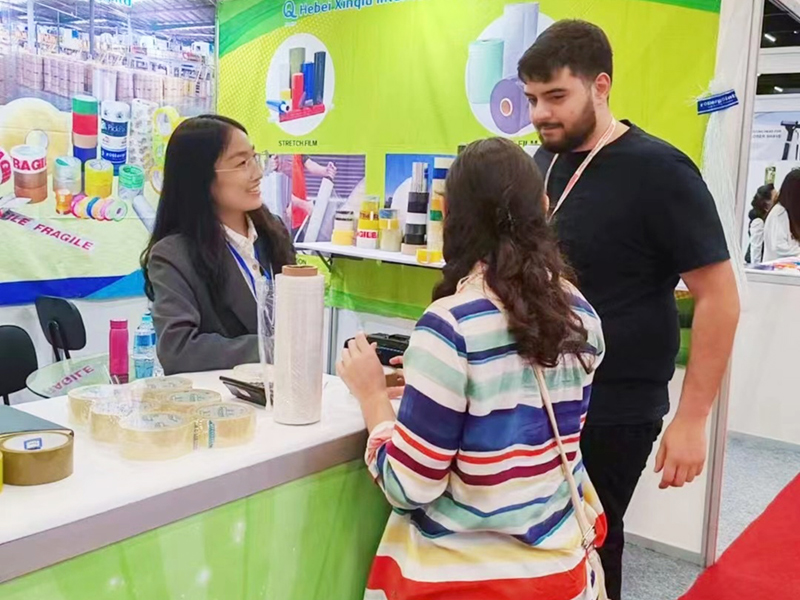
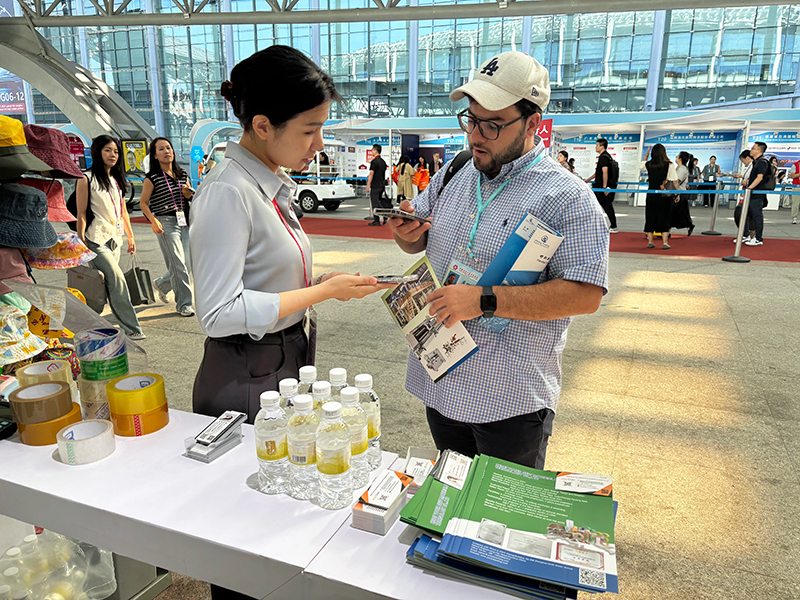
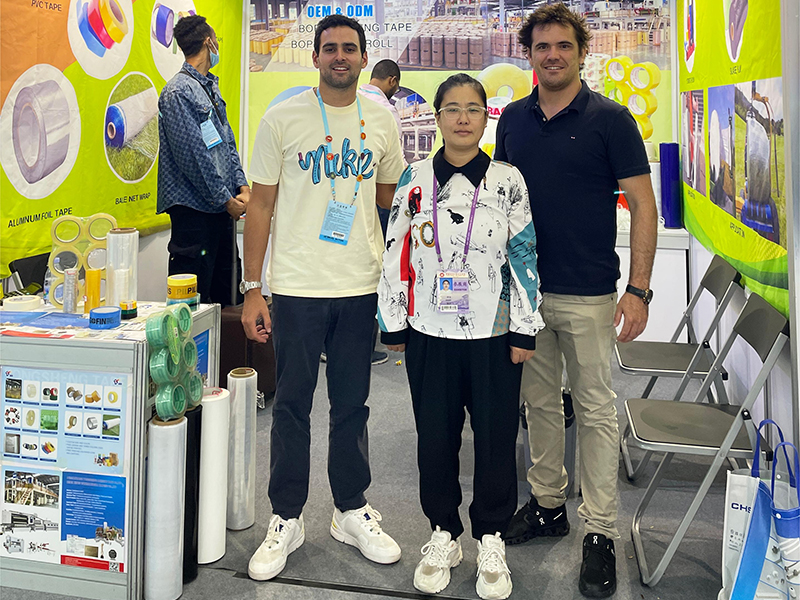
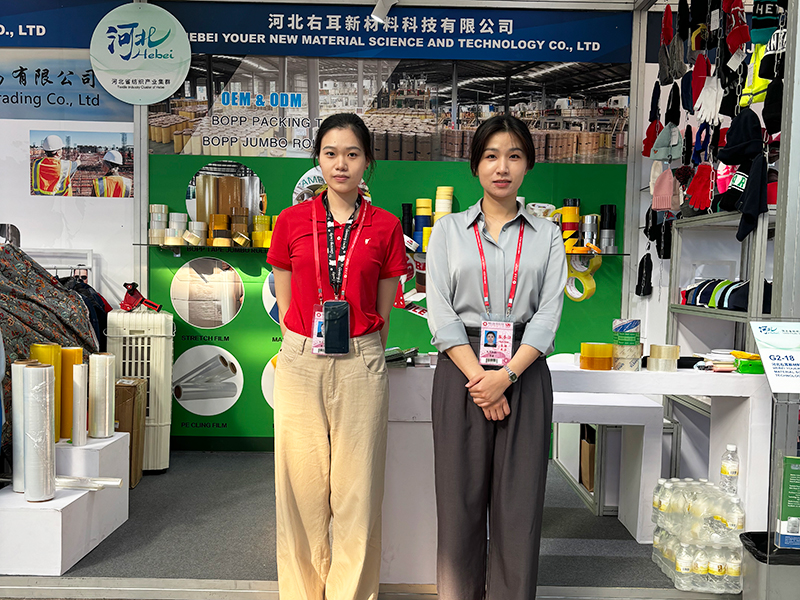
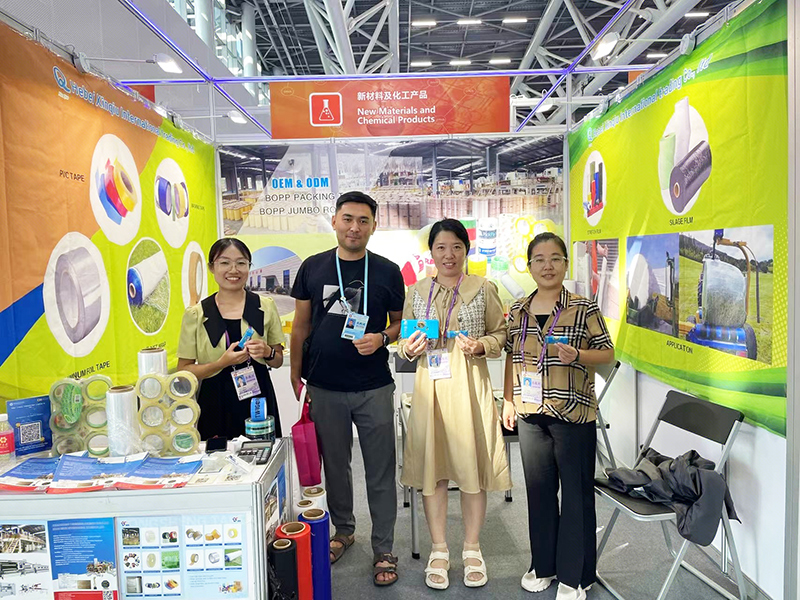
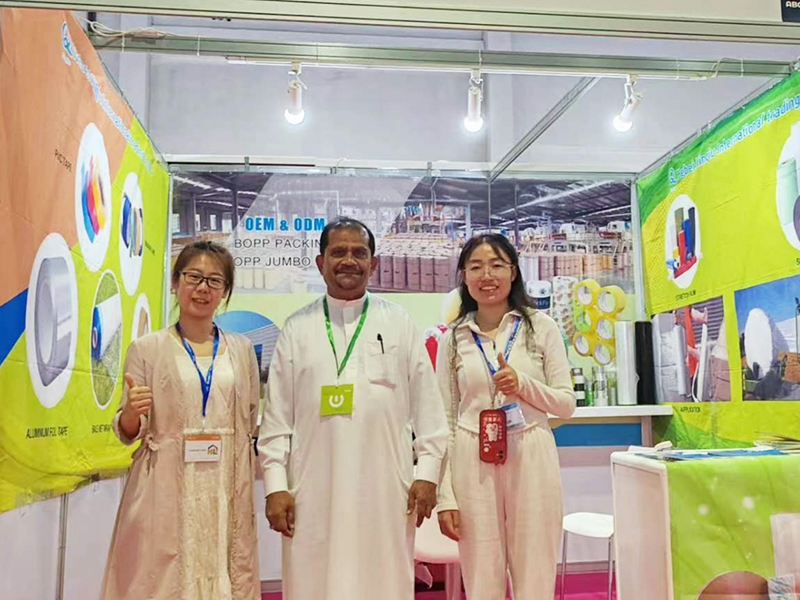
Meeting packaging professionals, logistics innovators, and supply chain leaders at international trade shows worldwide
Explore our full catalogue — engineered for every shipping and packaging challenge
Partner with Hebei Youer — your trusted HDPE film manufacturer serving 80+ countries. Request a custom quote, technical samples, or product specifications today.
Get a Free Quote & Sample →