- admin@youerfilms.com
- Mon - Sat at 9:00AM to 18:00PM
Leave Your Message
🏭
The global packaging industry is undergoing a massive transformation, and at the heart of this evolution is the Film Shrink Wrap for Food and Beverage Multipacks. As consumer demands shift towards convenience, bulk purchasing, and visual appeal, multipacks have become a dominant force in retail environments. From bottled water and canned sodas to bundled dairy products and snack packs, the reliance on high-quality shrink films has never been greater. Commercially, the market is driven by the need for cost-effective, lightweight, and durable packaging solutions that reduce the overall carbon footprint compared to traditional cardboard boxes.
Industrially, manufacturing facilities are scaling up operations to meet global supply chain demands. The shift towards automated packaging lines requires shrink films that offer superior tensile strength, consistent shrinkage rates, and excellent puncture resistance. Materials such as Polyolefin (POF), Polyethylene (PE), and Biaxially Oriented Polypropylene (BOPP) are being engineered at microscopic levels to ensure they perform flawlessly on high-speed wrapping machines. In the current landscape, efficiency is paramount. A single tear or inconsistent shrink can halt a production line, leading to significant financial losses. Therefore, the industrial standard demands films that guarantee seamless operability, exceptional clarity for branding, and robust protection during transit.
Furthermore, the economic implications of utilizing advanced shrink wrap films are profound. By minimizing material usage while maximizing load stability, beverage companies can significantly cut down on logistics and warehousing costs. The commercial sector is also witnessing a surge in customized printing on shrink films. With high-definition UV printing technology, shrink wraps are no longer just protective layers; they are powerful marketing canvases that grab consumer attention directly on the supermarket shelves.
Beverage Multipacks: The beverage industry is arguably the largest consumer of shrink wrap films. Whether it is a 6-pack of craft beer, a 24-pack of bottled water, or energy drink bundles, the film must provide structural integrity. PE heat shrinkable films are heavily utilized here due to their thick, durable nature that can bear the weight of heavy liquids. The film must tightly contour around the bottles or cans, preventing friction and potential breakage during global transit. Additionally, the outer packaging film serves as a barrier against dust, moisture, and UV rays, ensuring the product inside remains pristine.
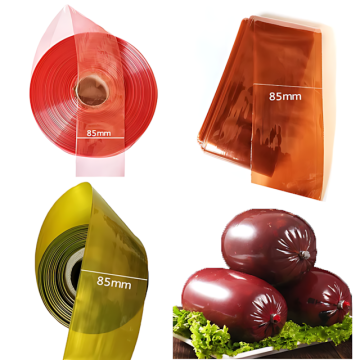
Perishable Food and Dairy: When dealing with perishable goods like sausages, cheese, and yogurt multipacks, the requirements shift towards barrier properties. Food Grade Polyamide Shrink Films are engineered to offer high oxygen barriers, which drastically extend the shelf life of the products. The soft, glossy finish not only enhances the visual appeal but also provides a hygienic seal that prevents contamination. In these scenarios, the shrink film acts as a crucial component of food safety, adhering strictly to FDA and international health standards.
Gourmet and Confectionery Bundling: For high-grade food packaging, aesthetics play a role equally as important as protection. BOPP Matte Films are frequently chosen for their premium, frosted appearance. They are used to bundle luxury chocolates, specialty teas, and artisanal snacks. The matte surface provides a sophisticated tactile experience and prevents glare under retail lighting, allowing the underlying brand graphics to stand out elegantly.
Logistics and Pallet Wrapping: Beyond the individual multipack, the entire pallet must be secured for distribution. High-quality LLDPE stretch films are deployed to wrap hundreds of multipacks together. This logistics packaging ensures that the food and beverage items do not shift, collapse, or suffer damage during forklift handling and long-haul transportation. The customizable stretchability and tear resistance of LLDPE make it an indispensable asset in the food supply chain.
🤖
The intersection of packaging and technology has birthed a new era of Smart Manufacturing. Artificial Intelligence (AI) and machine learning algorithms are now deeply integrated into the production lines of shrink wrap films. During the extrusion process, AI-driven sensors continuously monitor the thickness, opacity, and molecular alignment of the film. If a microscopic deviation occurs, the system automatically adjusts the machine parameters in real-time, ensuring that every roll of film meets exact specifications. This level of precision eliminates human error and drastically reduces material waste.
On the client side, food and beverage manufacturers are utilizing AI-powered vision systems on their packaging lines. These systems inspect the multipacks after they pass through the heat tunnel. The AI can instantly detect if the shrink wrap has any wrinkles, burn holes, or improper seals. If a defect is found, the specific multipack is automatically rejected from the line. Furthermore, predictive maintenance powered by AI helps factories foresee when packaging machinery needs servicing, thereby preventing unexpected downtime and ensuring a continuous flow of food and beverage products to the market.
Additionally, advanced polymer science has led to the development of self-healing and scratch-resistant properties in films. While traditionally used in automotive protection, these technologies are cross-pollinating into the food logistics sector, ensuring that the transparent protective films covering delicate food display cases or premium beverage gifts remain flawless despite rough handling.
🌱
As global awareness regarding plastic pollution intensifies, the future of Film Shrink Wrap for Food and Beverage Multipacks lies in sustainability. The industry is rapidly pivoting towards eco-friendly alternatives without compromising on performance. One major trend is the development of ultra-thin films. Through advanced co-extrusion technologies, manufacturers can create multi-layered films that are significantly thinner but possess the same, if not better, tensile strength as their thicker predecessors. This process, known as "downgauging," reduces the total volume of plastic used and lowers shipping weights, subsequently reducing carbon emissions.
Another profound trend is the integration of Post-Consumer Recycled (PCR) plastics into shrink films. By blending recycled resins with virgin polymers, companies are creating a circular economy loop. Furthermore, the push for fully biodegradable and compostable shrink wraps is gaining unprecedented momentum. Researchers are exploring bio-based polymers derived from corn starch and sugarcane that can provide the necessary heat-shrink properties for beverage multipacks while breaking down naturally in the environment after use. As regulatory frameworks tighten globally, adopting these sustainable film solutions is no longer just an ethical choice, but a commercial necessity for food and beverage brands.
Hebei Youer New Material Science and Technology Co., Ltd. has been founded since 2007. Located in Shijiazhuang City, Hebei Province, we have specialized in high-performance films for over a decade, evolving into a modern high-tech enterprise integrating R&D, production, and global sales.
Our product system focuses on three core product lines — stretch film, protective film, and BOPP film, with detailed extended classifications to fully cover the diverse and rigorous application needs of the food, beverage, and logistics industries.
With profound experience in product development and materials exporting, we have gained a stellar reputation among clients worldwide. Our professional sales team is always ready to provide quick responses and multi-choice, one-stop services to satisfy complex customer requirements.
We strictly implement international quality control standards throughout the entire production process, from the selection of high-quality raw materials to the precision testing of finished products, forming a complete quality management system. Every roll of film leaving the factory has undergone strict AI-assisted inspection to ensure that it meets the highest quality requirements of our global customers.
We have built a professional R&D team composed of senior engineers and technical talents, equipped with advanced R&D and testing equipment. We focus on technological breakthroughs and product upgrading, continuously developing environmentally friendly, efficient, and high-performance film products to keep pace with changing market demands and lead the industry's development trend.
Our vision is to become a world-class film manufacturer, promote the sustainable development of the packaging industry, and create greater value for customers, employees, and society through continuous innovation. We look forward to building long-term partnerships with potential customers all over the world.
Our commitment to excellence is recognized globally. We actively participate in international packaging exhibitions to showcase our latest innovations in shrink wrap technology.