- admin@youerfilms.com
- Mon - Sat at 9:00AM to 18:00PM
Leave Your Message
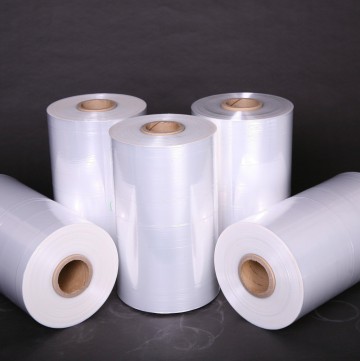
Explore our core product lineup — each film engineered for specific multipack bundling, food-contact safety, and high-speed line performance.
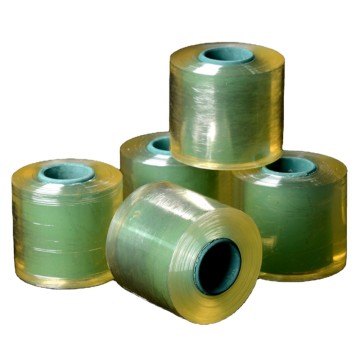
Clear PVC (Polyvinyl Chloride) shrink film has long been the backbone of multipack packaging in the global food and beverage industry. Its exceptional optical clarity, controlled shrink properties, and robust mechanical performance make it the preferred choice for bundling bottles, cans, cartons, and trays at high production speeds. Whether it's a 6-pack of mineral water, a 12-pack of sparkling beverages, or a multi-unit snack tray, clear PVC film delivers the tightly conforming, visually transparent wrap that retailers and consumers expect.
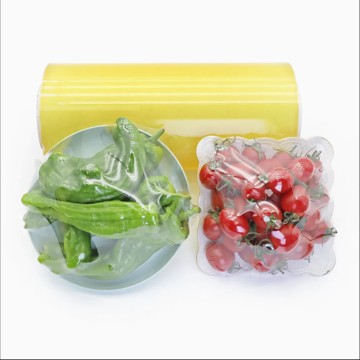
Unlike opaque alternatives, clear PVC film allows full product visibility on the shelf — a critical commercial advantage in today's competitive retail landscape where packaging is itself a marketing tool. Consumers can see the product, verify the quantity, and assess quality without opening the bundle. This transparency translates directly into purchase confidence and brand trust.
The global food and beverage multipack packaging market is valued at over USD 42 billion and continues to grow at a CAGR of approximately 4.8% through 2030. Within this market, shrink films — especially clear PVC variants — account for a dominant share of rigid multipack bundling applications. Key commercial sectors include:
The packaging film industry is undergoing rapid transformation driven by sustainability imperatives, e-commerce growth, and automation. Here are the most significant trends impacting clear PVC film for food and beverage multipacks:
Manufacturers are under constant pressure to reduce material consumption without compromising performance. Advanced PVC film formulations now allow gauge reduction from traditional 40–50 microns down to 25–30 microns while maintaining equivalent tensile strength and shrink force. This lightweighting reduces raw material costs, lowers carbon footprint per pack, and improves line efficiency through faster heat transfer in shrink tunnels.
While PVC has faced scrutiny in some markets due to recycling challenges, the industry has responded with chlorine-free PVC alternatives and improved mono-material film structures. Leading film producers are investing in take-back schemes and closed-loop recycling partnerships with major FMCG brands. Additionally, the development of bio-based plasticizers has reduced the environmental impact of PVC film production significantly.
Modern beverage filling and packaging lines operate at unprecedented speeds. Clear PVC film is being engineered with tighter shrink temperature windows (typically 75–120°C) and more consistent gauge tolerances (±2 microns) to ensure reliable performance on servo-driven shrink wrappers and heat tunnels without film breaks or misalignment.
For chilled and frozen multipack applications, anti-fog coatings on clear PVC film prevent condensation buildup that would obscure product visibility in refrigerated retail cases. Anti-slip additives improve pallet stability during warehousing and logistics, reducing product damage rates by up to 35%.
The integration of QR codes, NFC tags, and augmented reality triggers on multipack PVC film is emerging as a key differentiator. Clear film's optical properties allow printed codes to be scanned through the film layer, enabling supply chain traceability, consumer engagement campaigns, and anti-counterfeiting measures without additional labeling.
This is the highest-volume application for clear PVC shrink film globally. PET water bottles, juice bottles, and carbonated drink containers are grouped and conveyed through a seamer and heat shrink tunnel where PVC film wraps tightly around the bundle. The key requirements are: consistent shrink force to avoid bottle deformation, sufficient tensile strength to support stacking loads of 200–400 kg, and optical clarity to maintain brand label visibility. Our PVC films achieve zero-haze bundling even on embossed bottle surfaces.
The craft beer sector demands premium packaging aesthetics. Clear PVC film allows the distinctive label artwork of craft breweries to remain fully visible in the multipack format, eliminating the need for secondary cardboard carriers in many SKUs. The film must also resist condensation in chilled display cases — a requirement met by our anti-fog grade PVC film with specialized surfactant coatings that maintain clarity at 2–8°C retail temperatures.
Yogurt cups, butter portions, and fresh cheese multipacks present unique challenges: irregular heights, varying container diameters, and strict hygiene requirements. Clear PVC film's excellent conformability allows it to wrap mixed-height trays without tunneling or fisheyes. Food-contact grade formulations with no plasticizer migration ensure compliance with dairy product regulations in the EU, US, and Asian markets.
Retail-ready multipack formats for snacks benefit from PVC film's ability to be printed with promotional messaging (e.g., "Buy 3, Save 20%") while maintaining the transparent window that lets consumers see the product. Anti-static grades prevent dust attraction on the film surface, maintaining a clean retail presentation throughout the product's shelf life.
For warehouse clubs and bulk retail formats (24-pack, 36-pack), heavy-gauge PVC film (50–80 microns) provides the structural integrity needed for pallet-height stacking. Reinforced film formulations with enhanced puncture resistance protect against sharp container edges during mechanical handling, reducing shrinkage losses in distribution by up to 28%.
| Property | Clear PVC Film | POF Shrink Film | PE Stretch Film | OPS Film |
|---|---|---|---|---|
| Optical Clarity | ⭐⭐⭐⭐⭐ Excellent | ⭐⭐⭐⭐ Very Good | ⭐⭐⭐ Good | ⭐⭐⭐⭐ Very Good |
| Shrink Range | 40–70% TD | 50–80% TD | N/A (stretch) | 50–65% TD |
| Food-Contact Grade | ✅ Yes | ✅ Yes | ✅ Yes | ✅ Yes |
| Cold-Chain Performance | ⭐⭐⭐⭐⭐ | ⭐⭐⭐⭐ | ⭐⭐⭐⭐ | ⭐⭐⭐ |
| Cost Efficiency | ⭐⭐⭐⭐⭐ Lowest | ⭐⭐⭐ Medium | ⭐⭐⭐⭐ Low | ⭐⭐⭐ Medium |
| Printability | ⭐⭐⭐⭐⭐ | ⭐⭐⭐⭐ | ⭐⭐⭐ | ⭐⭐⭐⭐ |
| Recyclability | ⭐⭐⭐ Improving | ⭐⭐⭐⭐ | ⭐⭐⭐⭐⭐ | ⭐⭐⭐ |
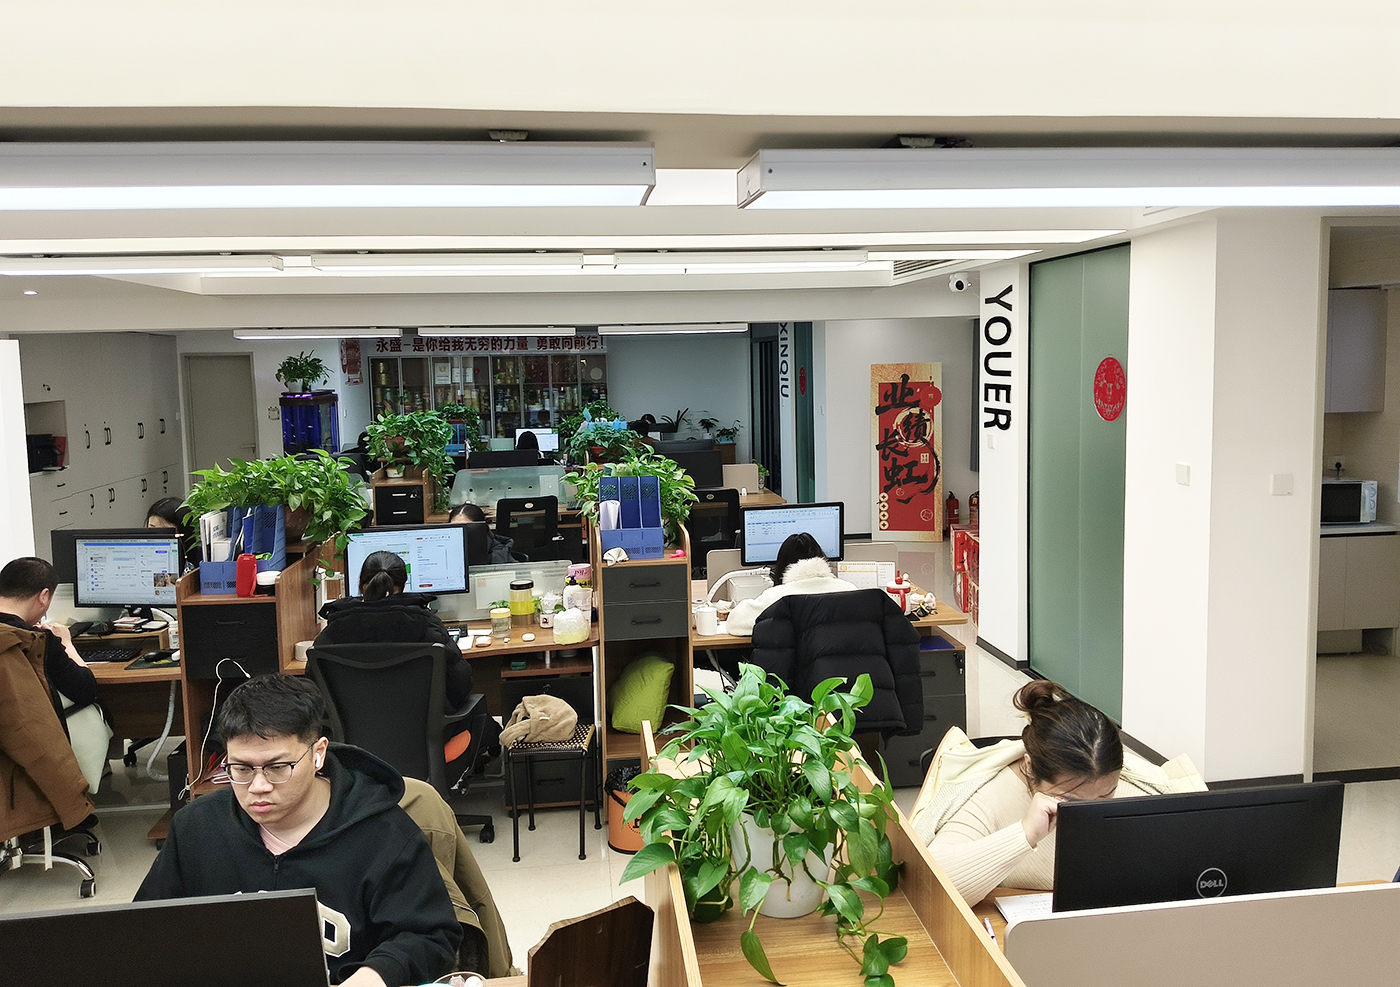
Hebei Youer New Material Science and Technology Co., Ltd. has been founded since 2007. Located in Shijiazhuang City, Hebei Province, we have specialized in film manufacturing for more than 10 years and have grown into a modern high-tech enterprise integrating R&D, production, and sales.
Our product system focuses on three core product lines — stretch film, protective film, and BOPP film — with detailed extended classifications to fully cover the diverse application needs of various industries, including food and beverage multipack packaging, industrial protection, and consumer goods bundling.
With deep experience in product development and materials exporting, we have gained an excellent reputation among customers from more than 80 countries. Our professional sales team is always ready to provide quick responses, multi-choice solutions, and one-stop service to satisfy all customer requirements.
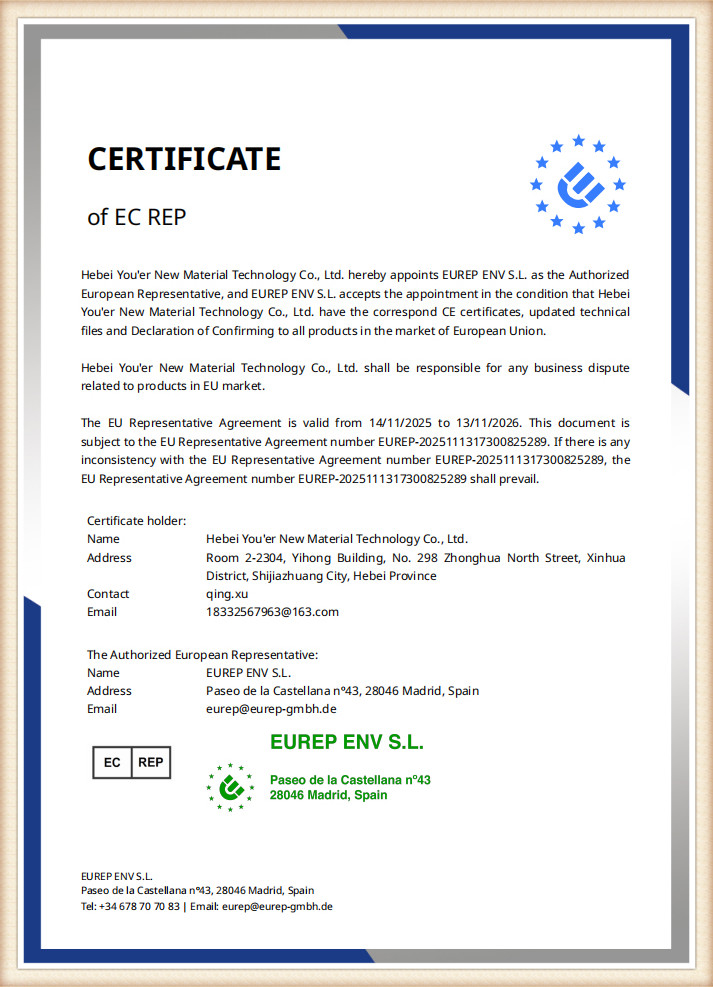
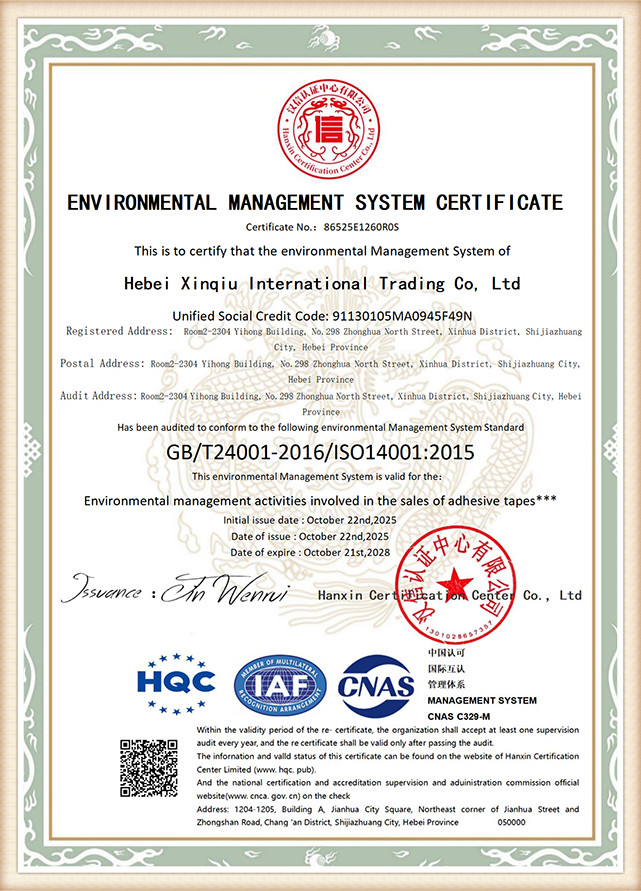
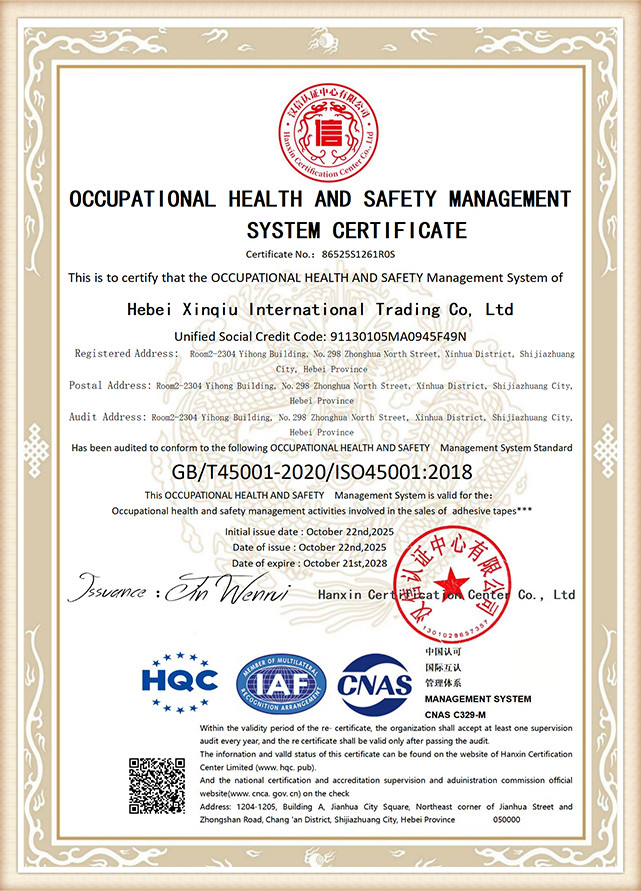
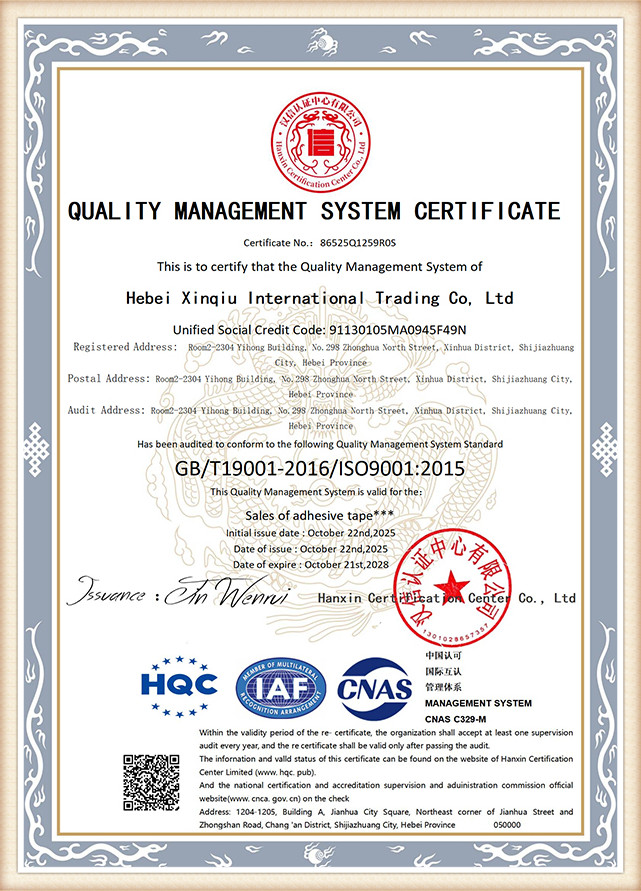
Our clear PVC films for food and beverage multipacks are backed by internationally recognized certifications, ensuring compliance with global food safety and quality standards.
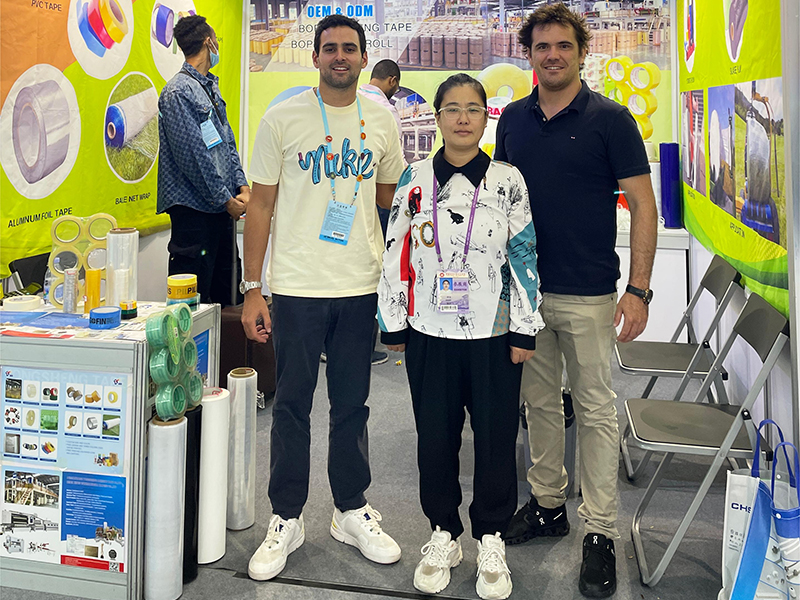
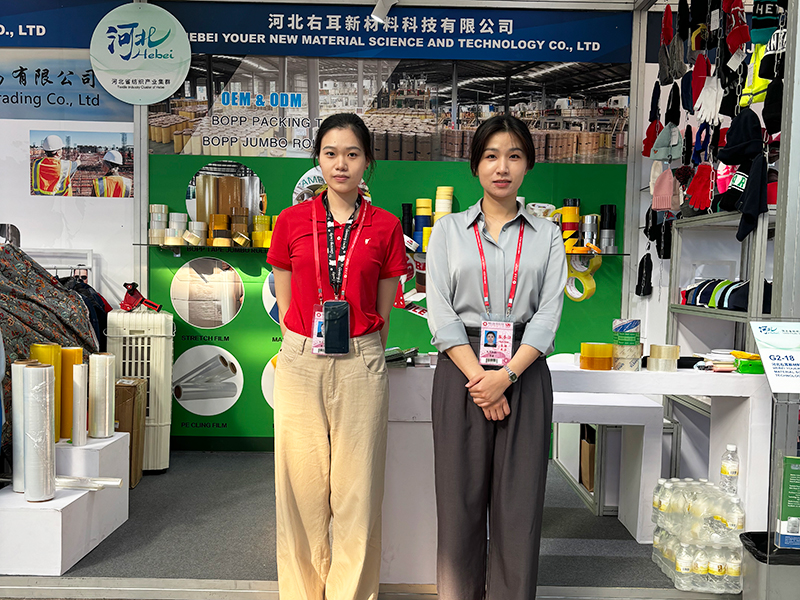
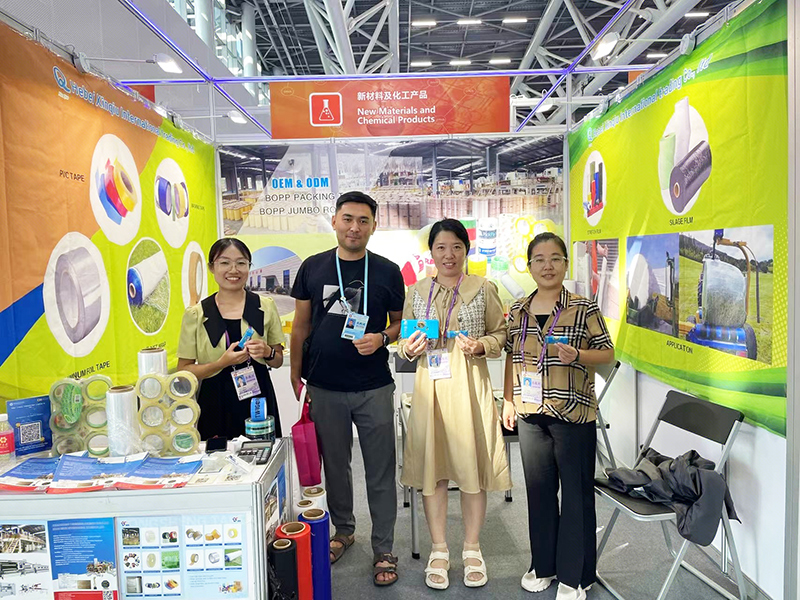
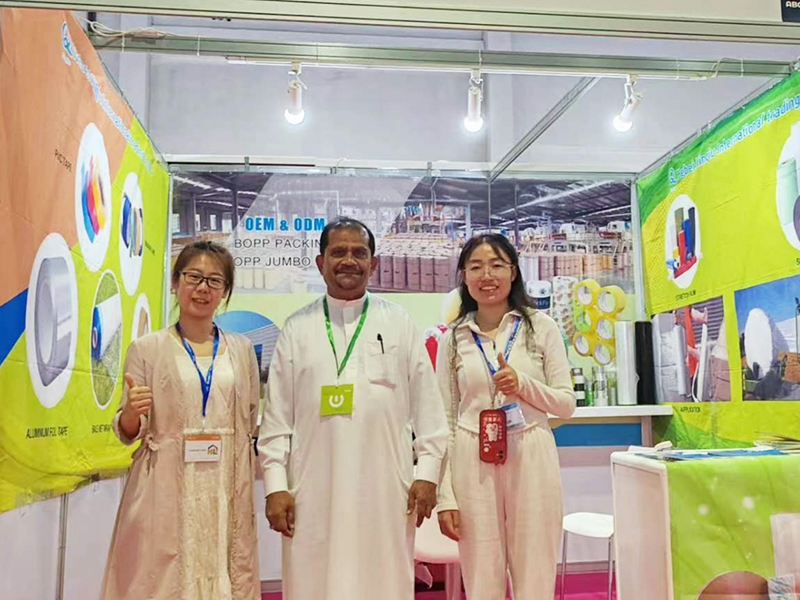
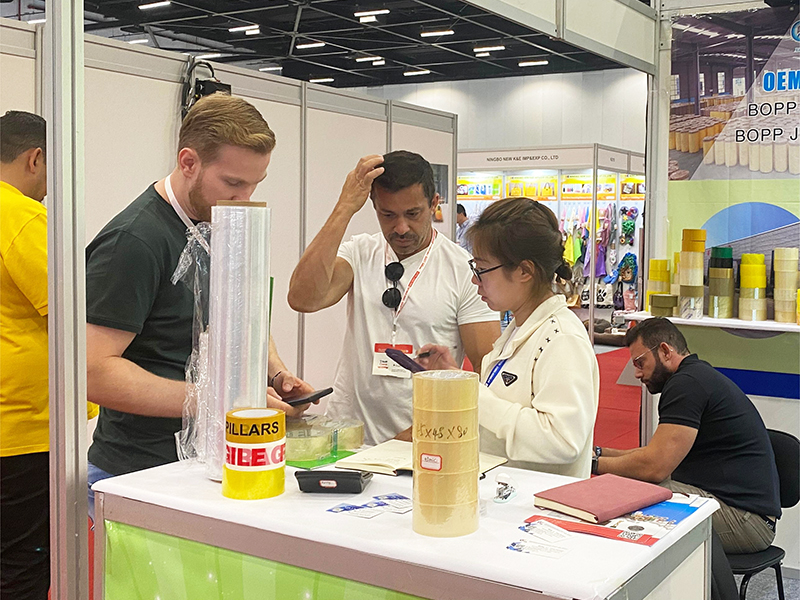
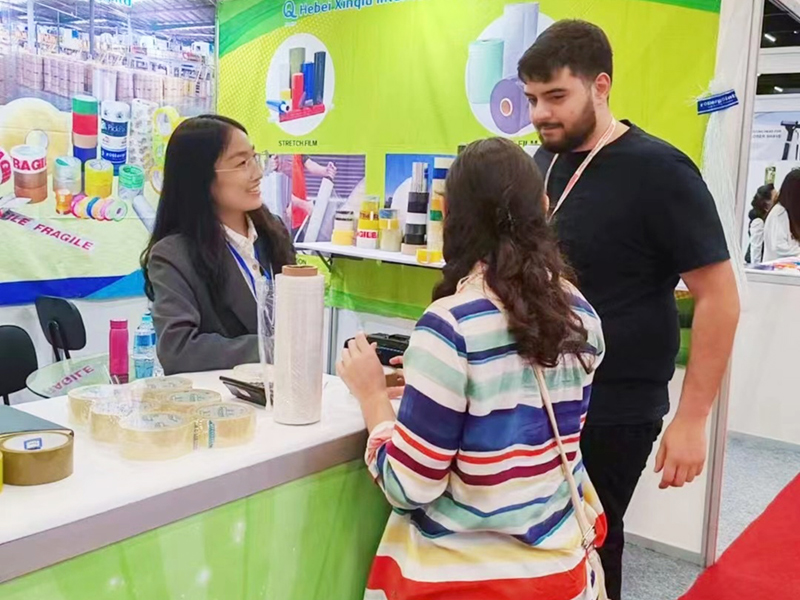
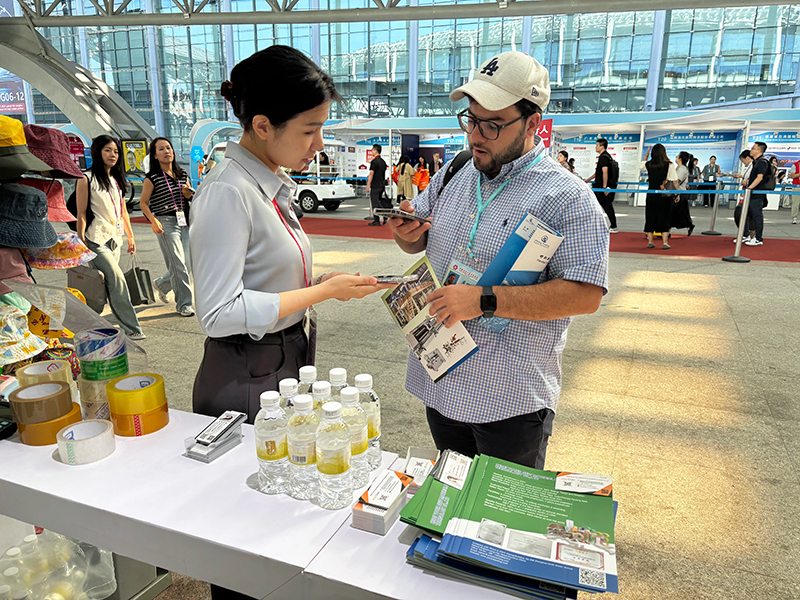
We actively participate in international packaging and food industry exhibitions, showcasing our latest clear PVC film innovations for food and beverage multipack applications to global partners.
Beyond clear PVC multipack film, our complete product portfolio covers every protective, bundling, and specialty film need across the food, beverage, and industrial sectors.